WhatsApp
wechat qr
Chat
Email
Message
Back to Top

Industrial Pumps

Heavy-Duty Industrial Pumps For Water, Chemicals, Slurry, Demanding Applications.

Handle water, chemicals, slurry and other industrial fluids with HRZL pumps. Select the right pump based on flow, head, fluid properties and operating conditions for mining, chemical processing, power generation and water supply.

Find the Right Industrial Pump

Water | Dewatering | Fire | Chemical | Slurry | Wastewater | Power
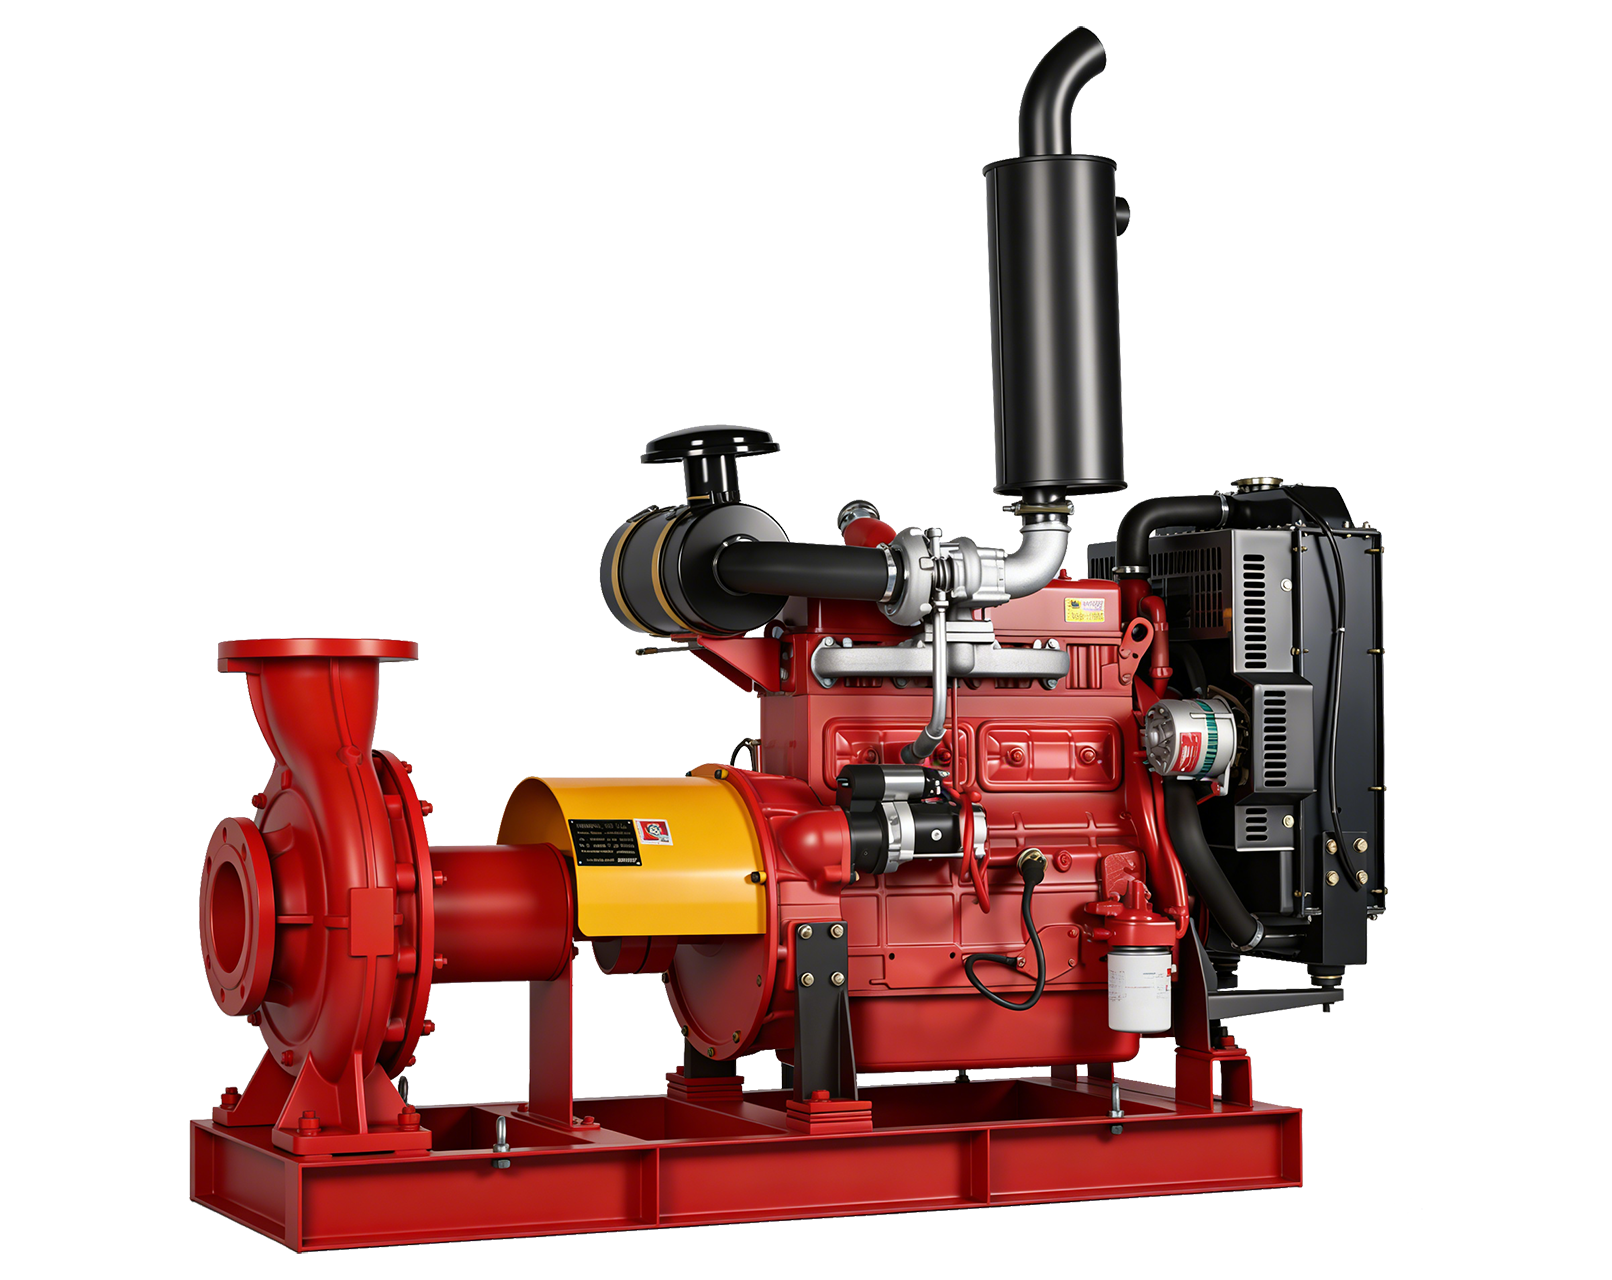
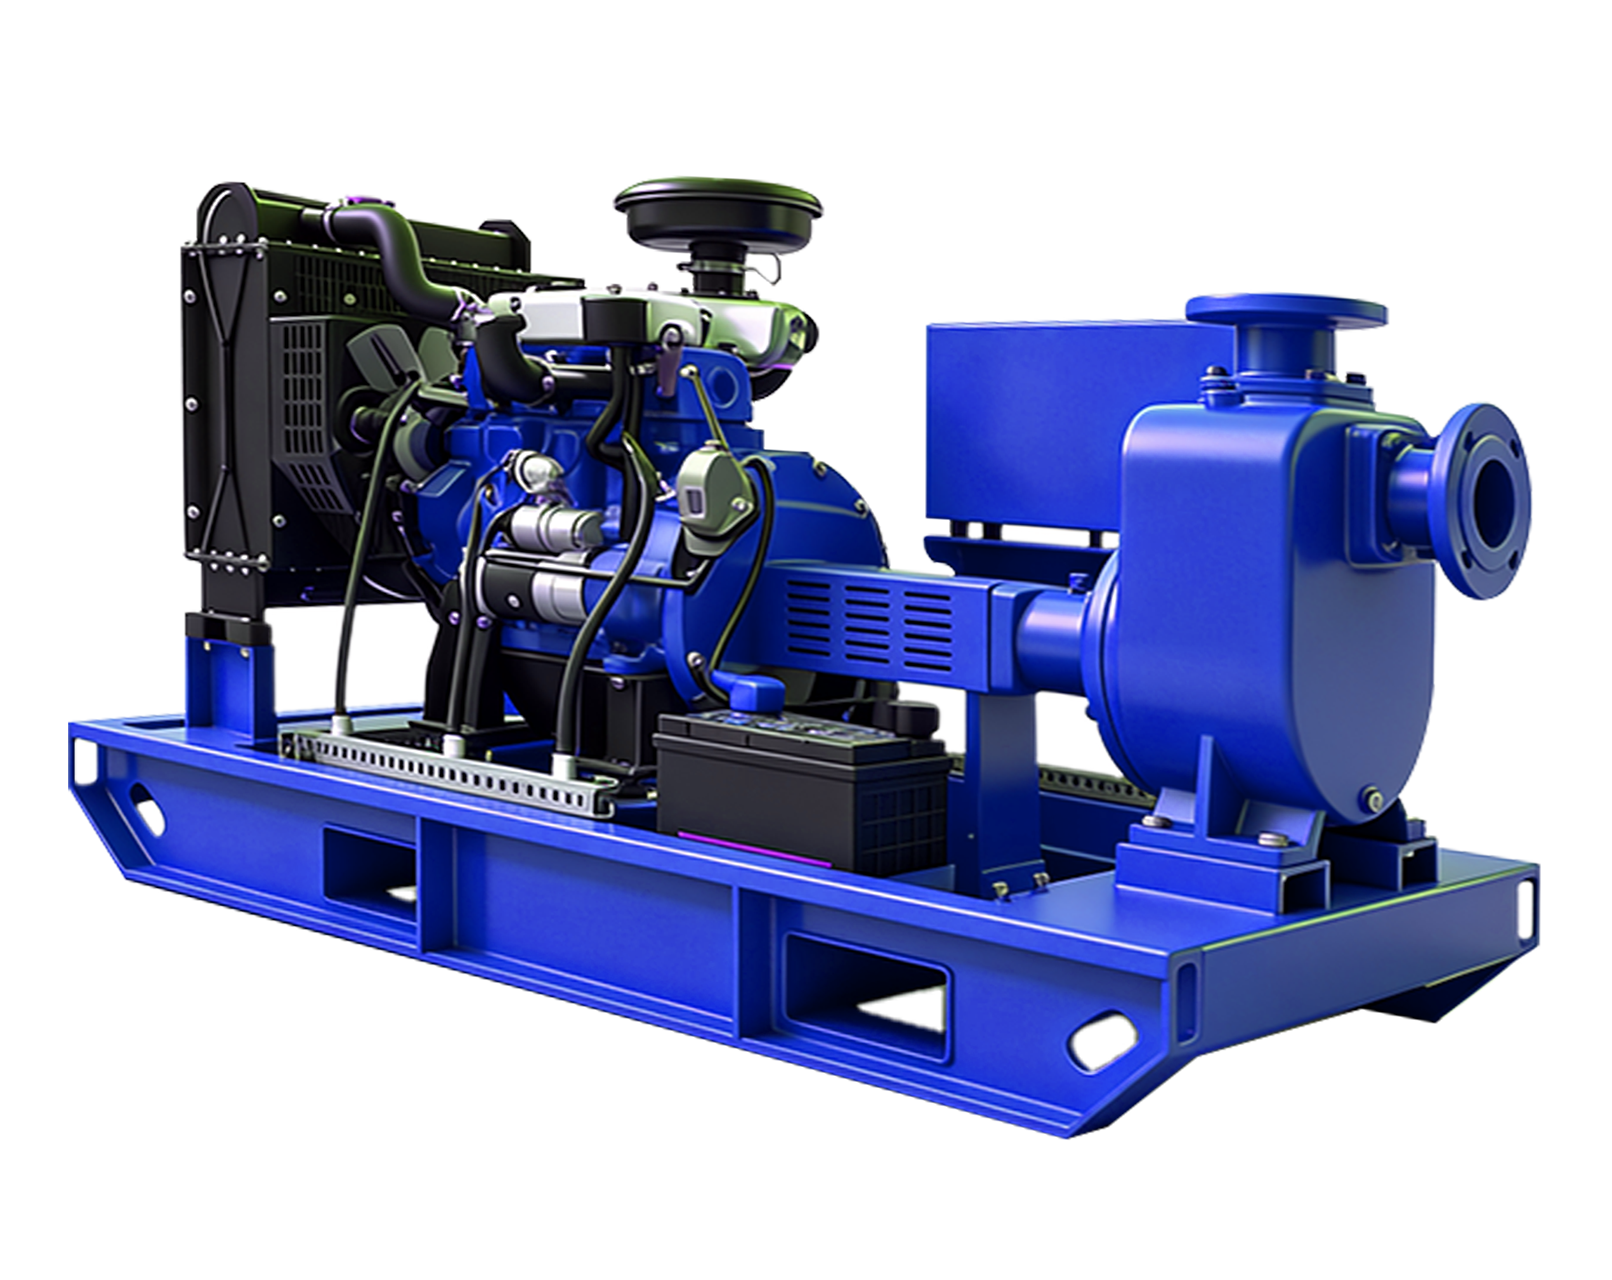
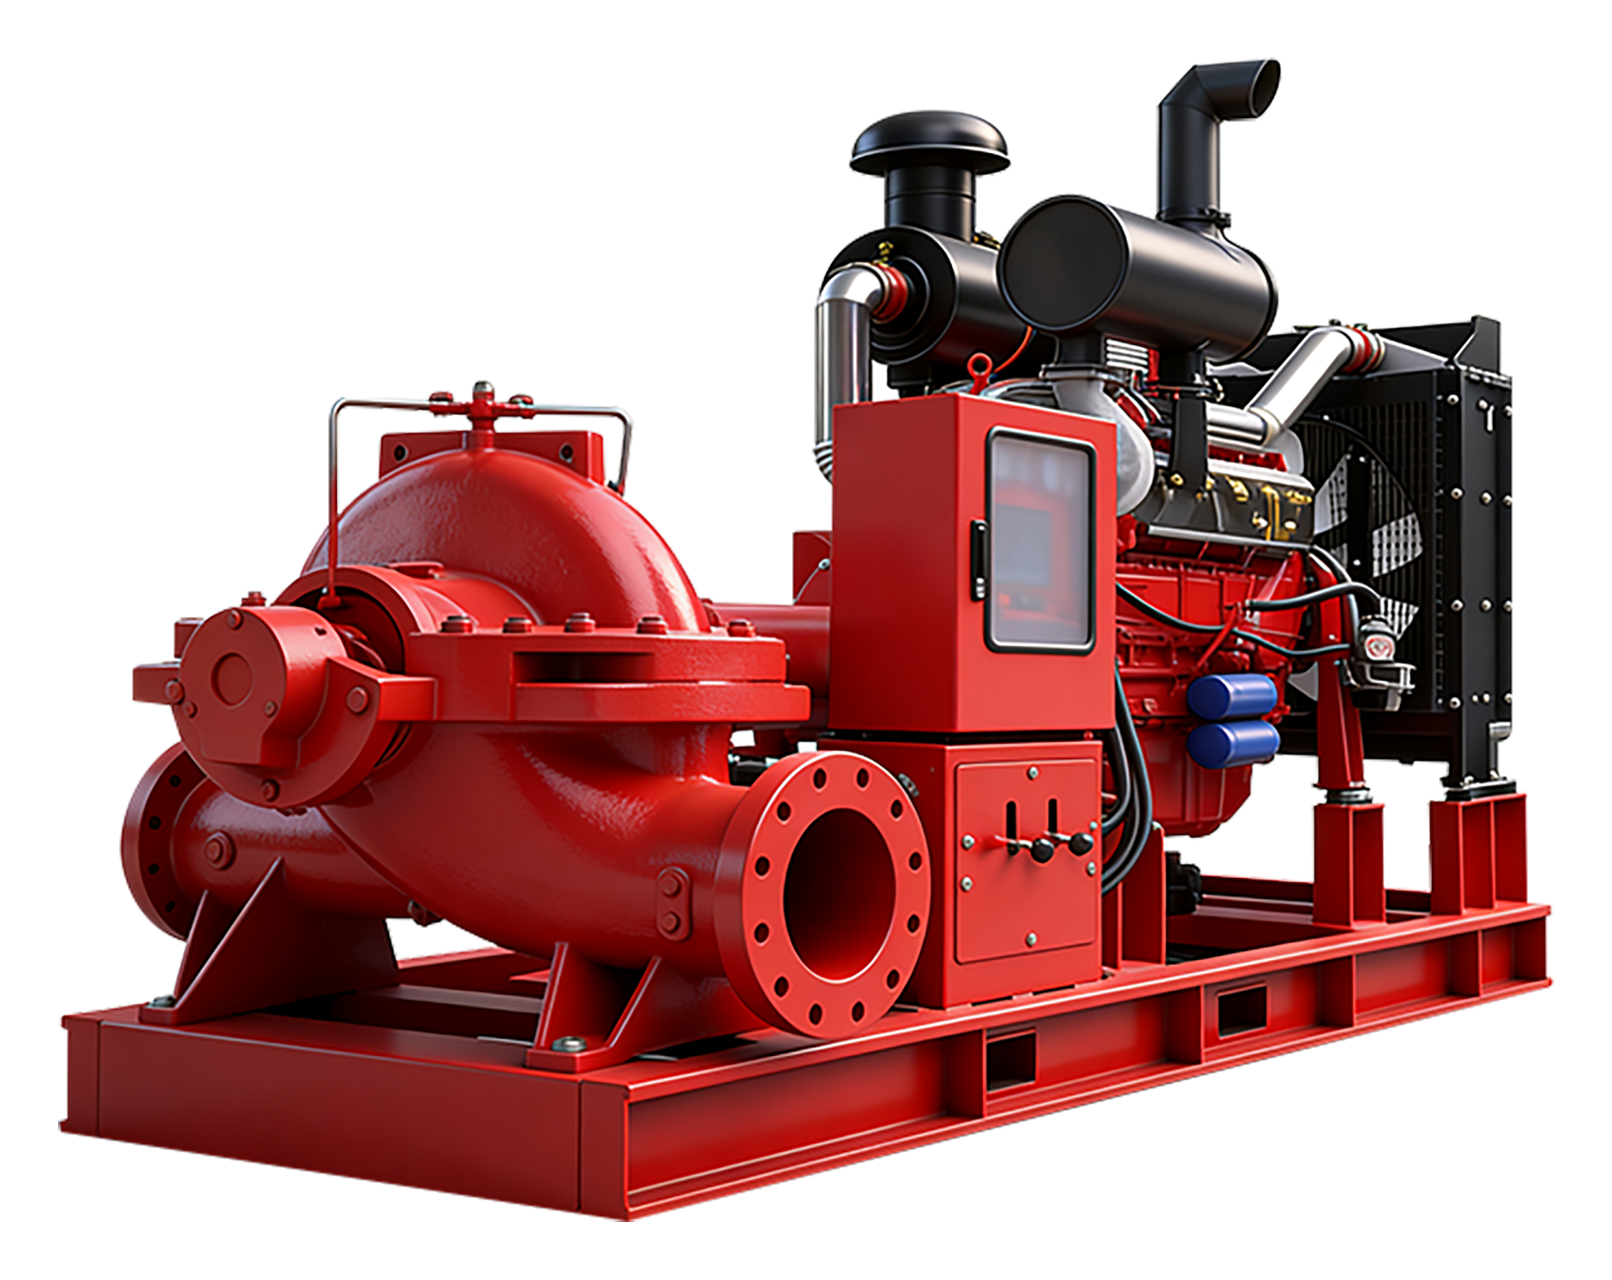
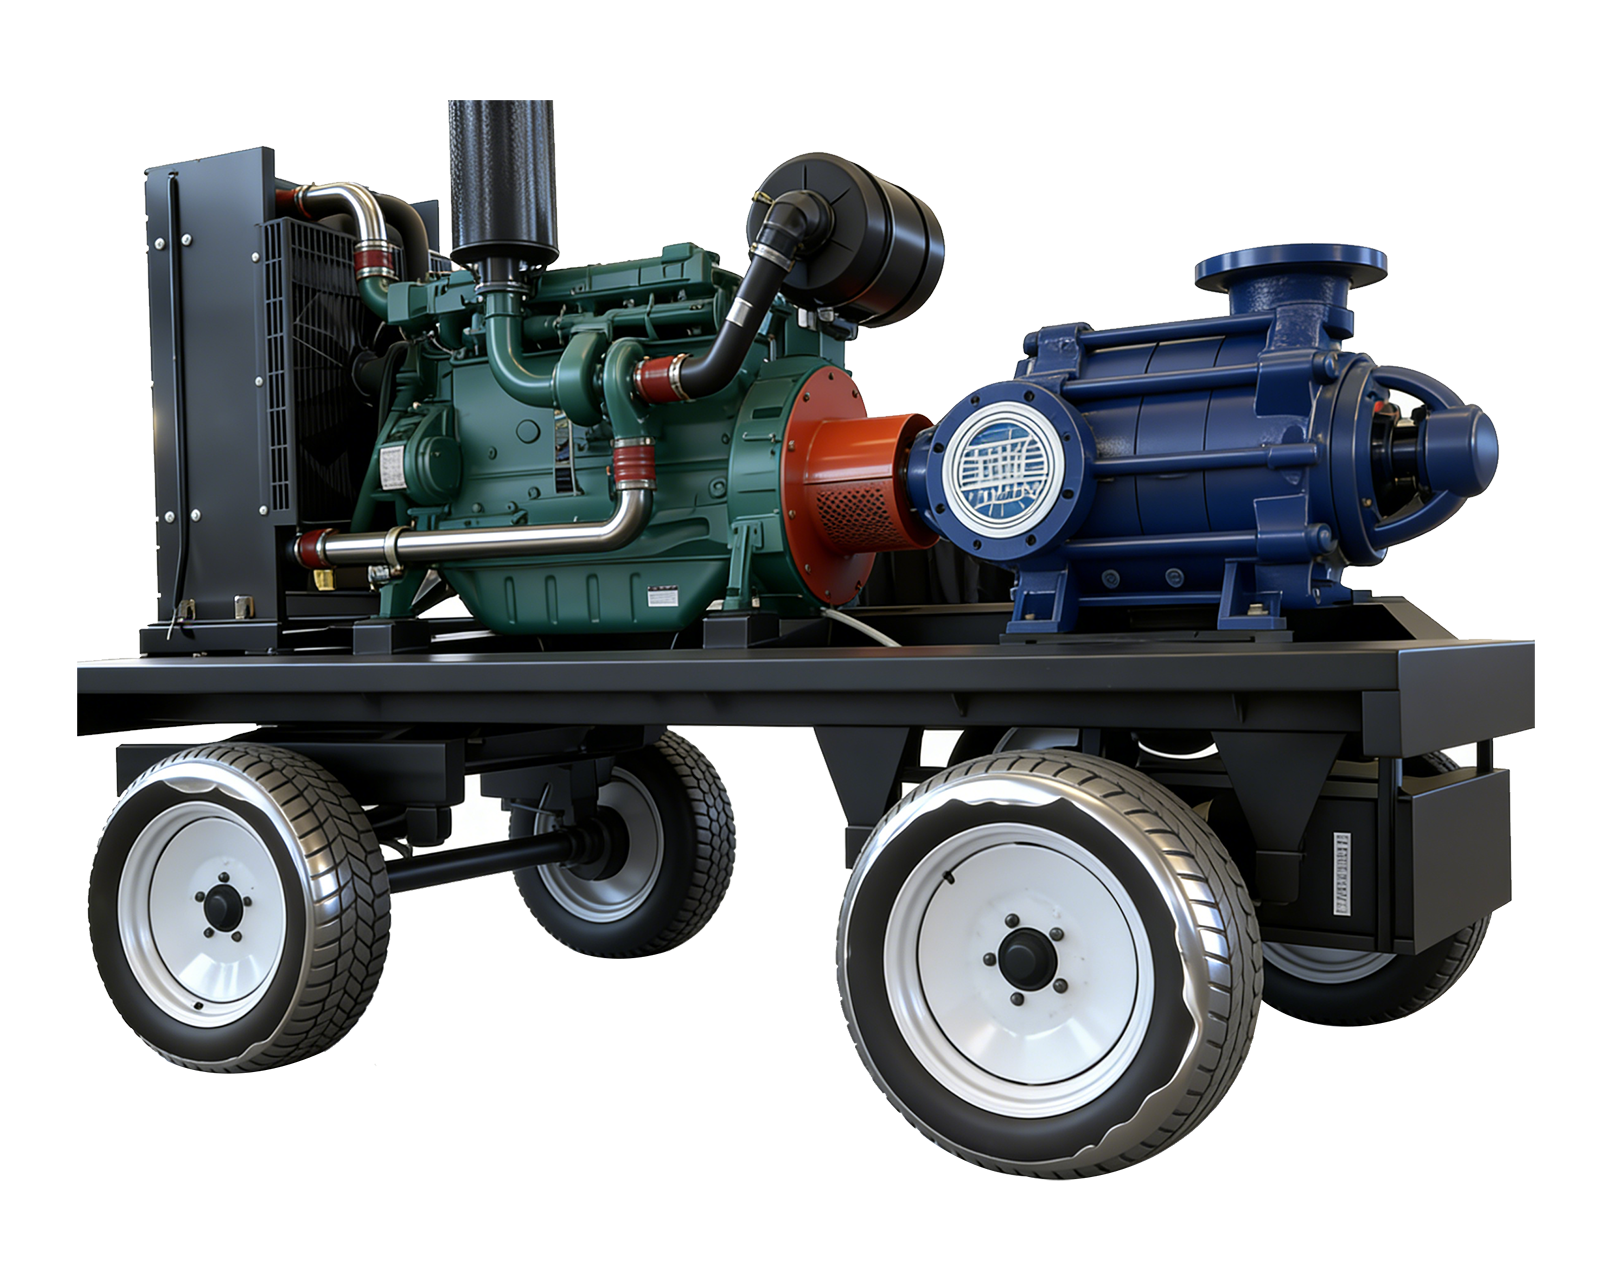
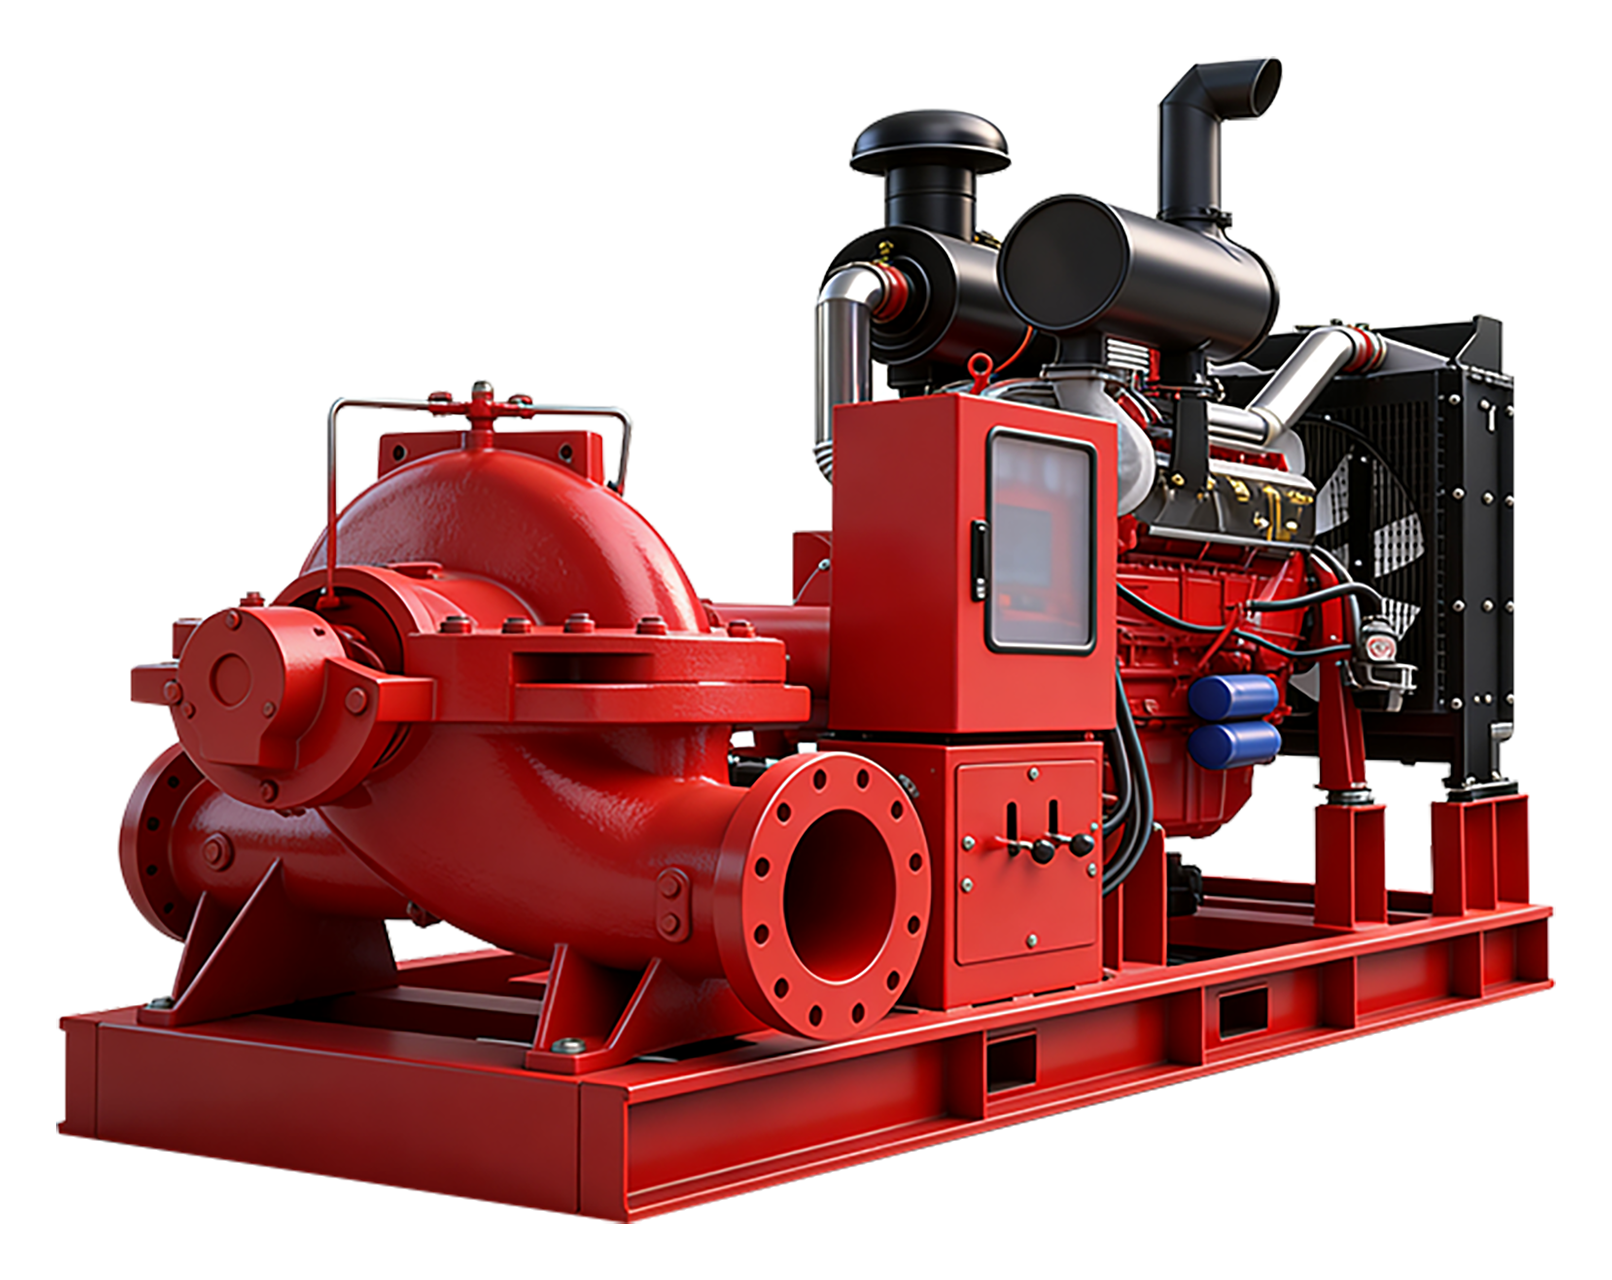
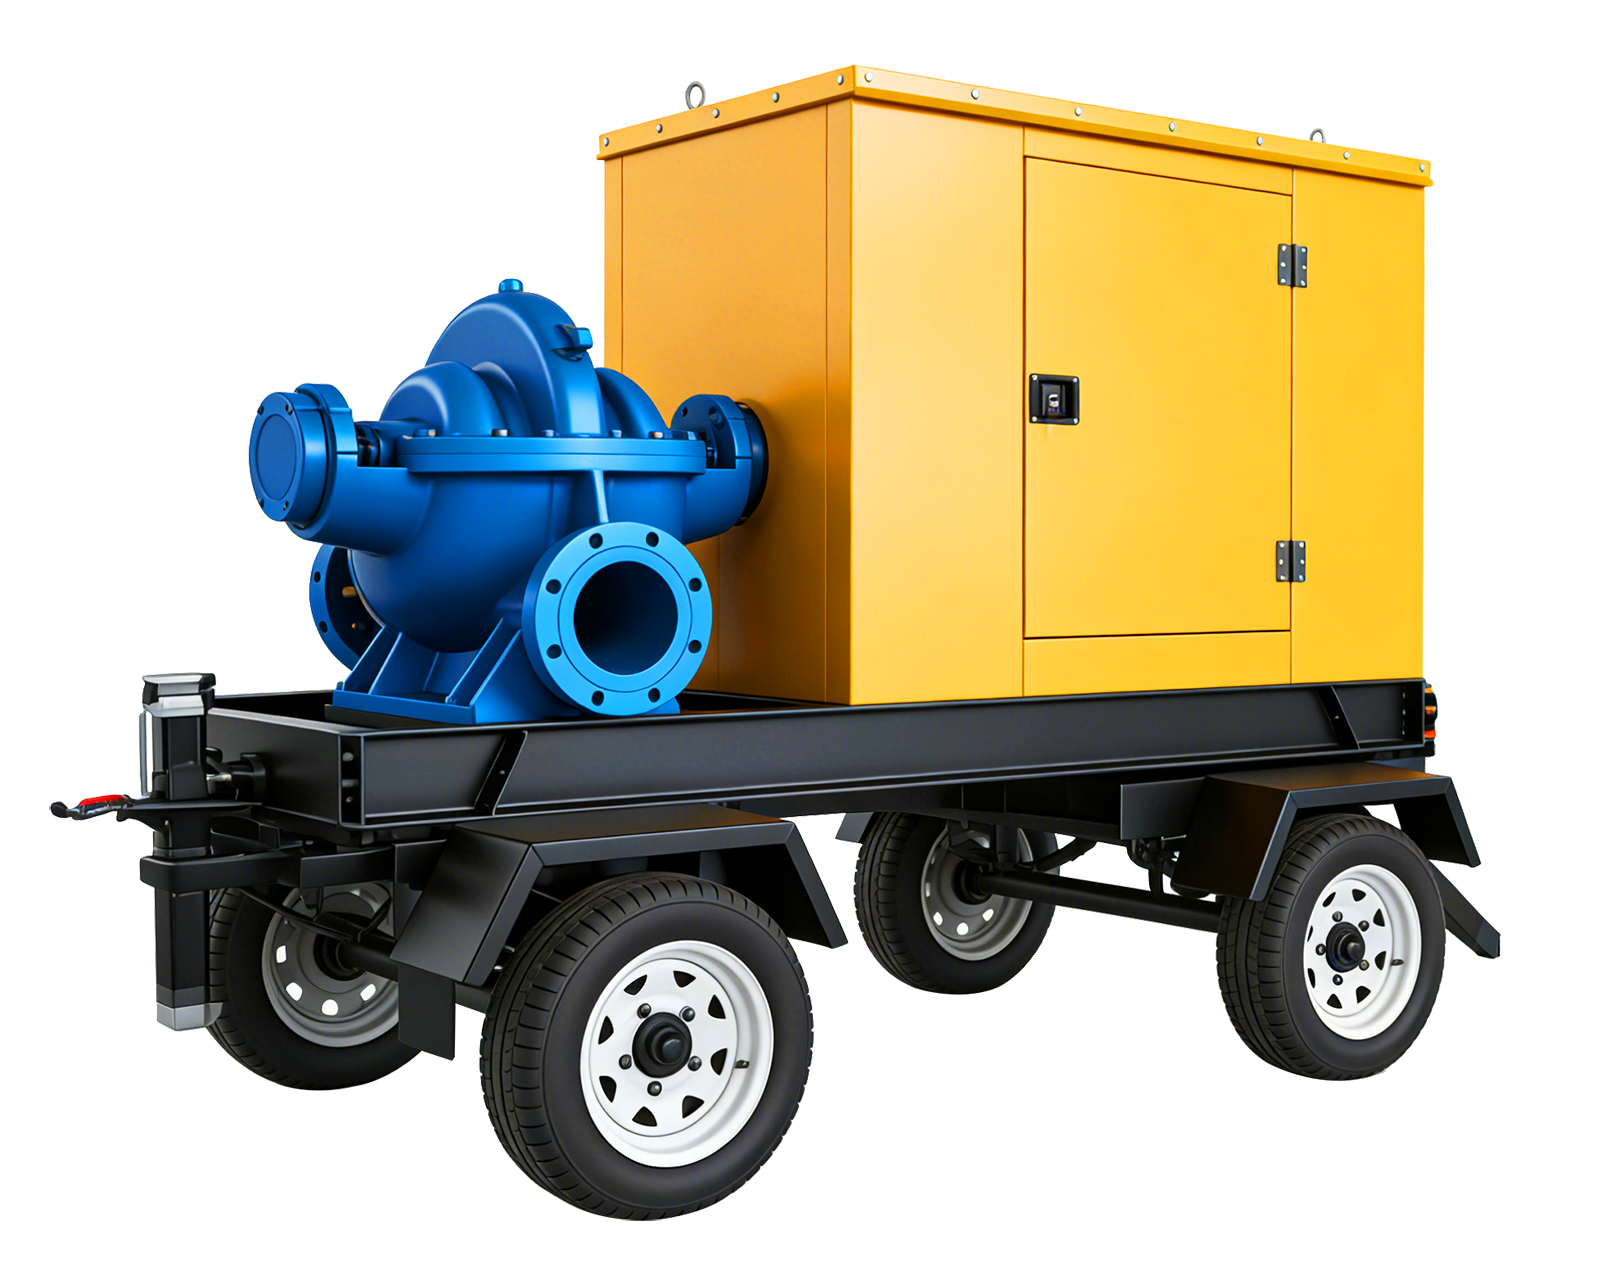
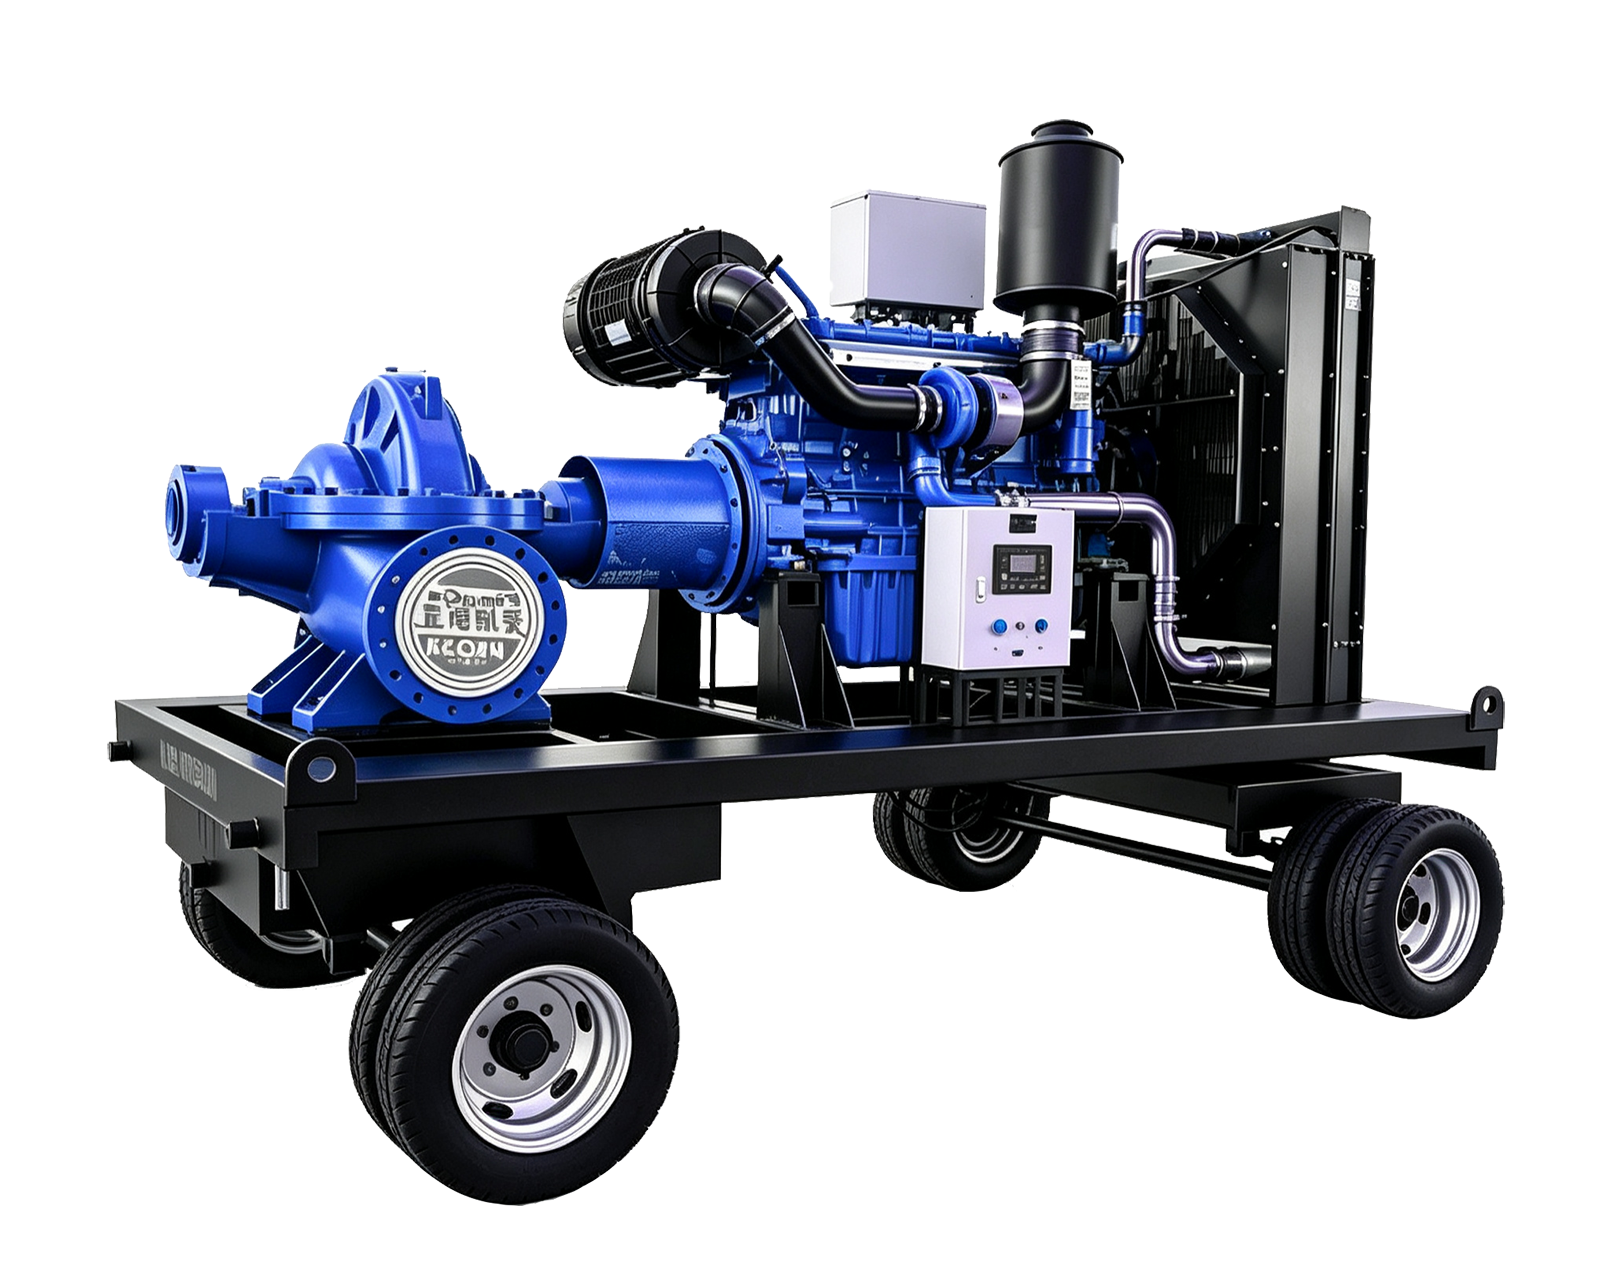
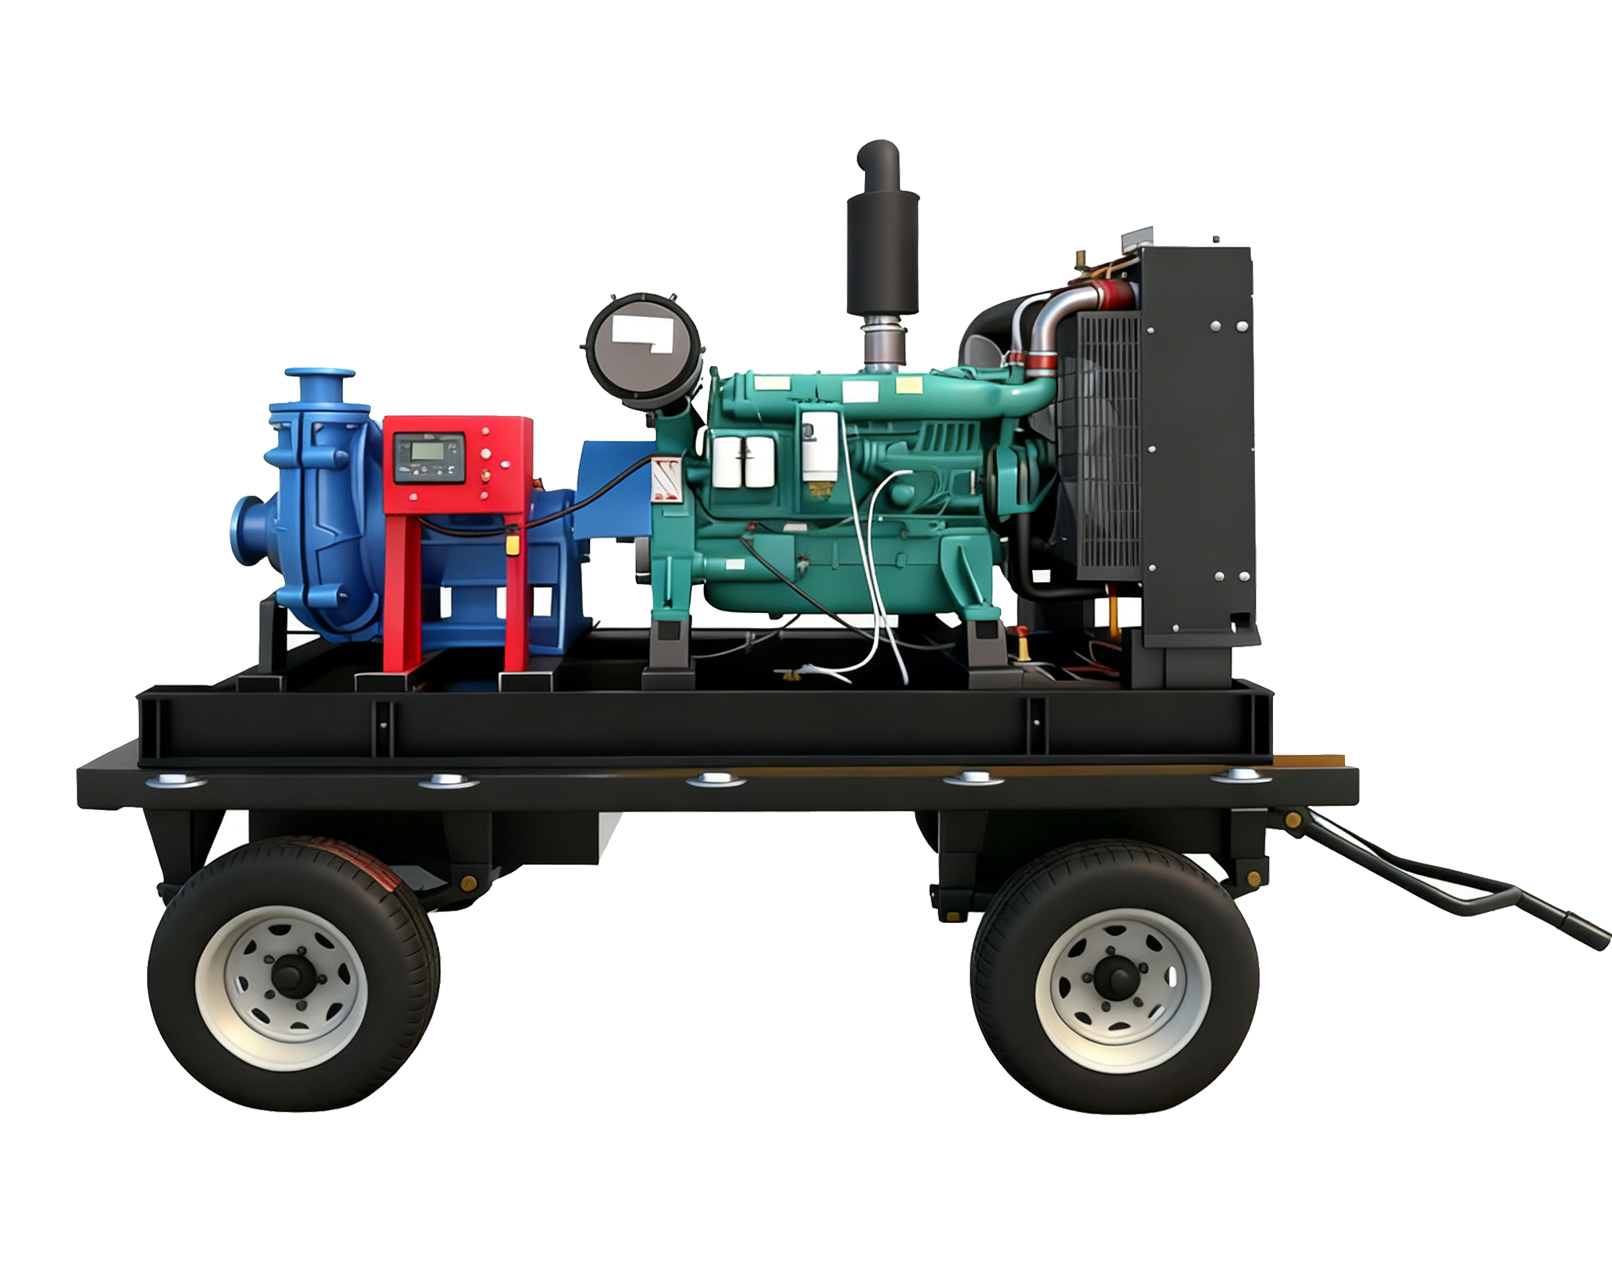
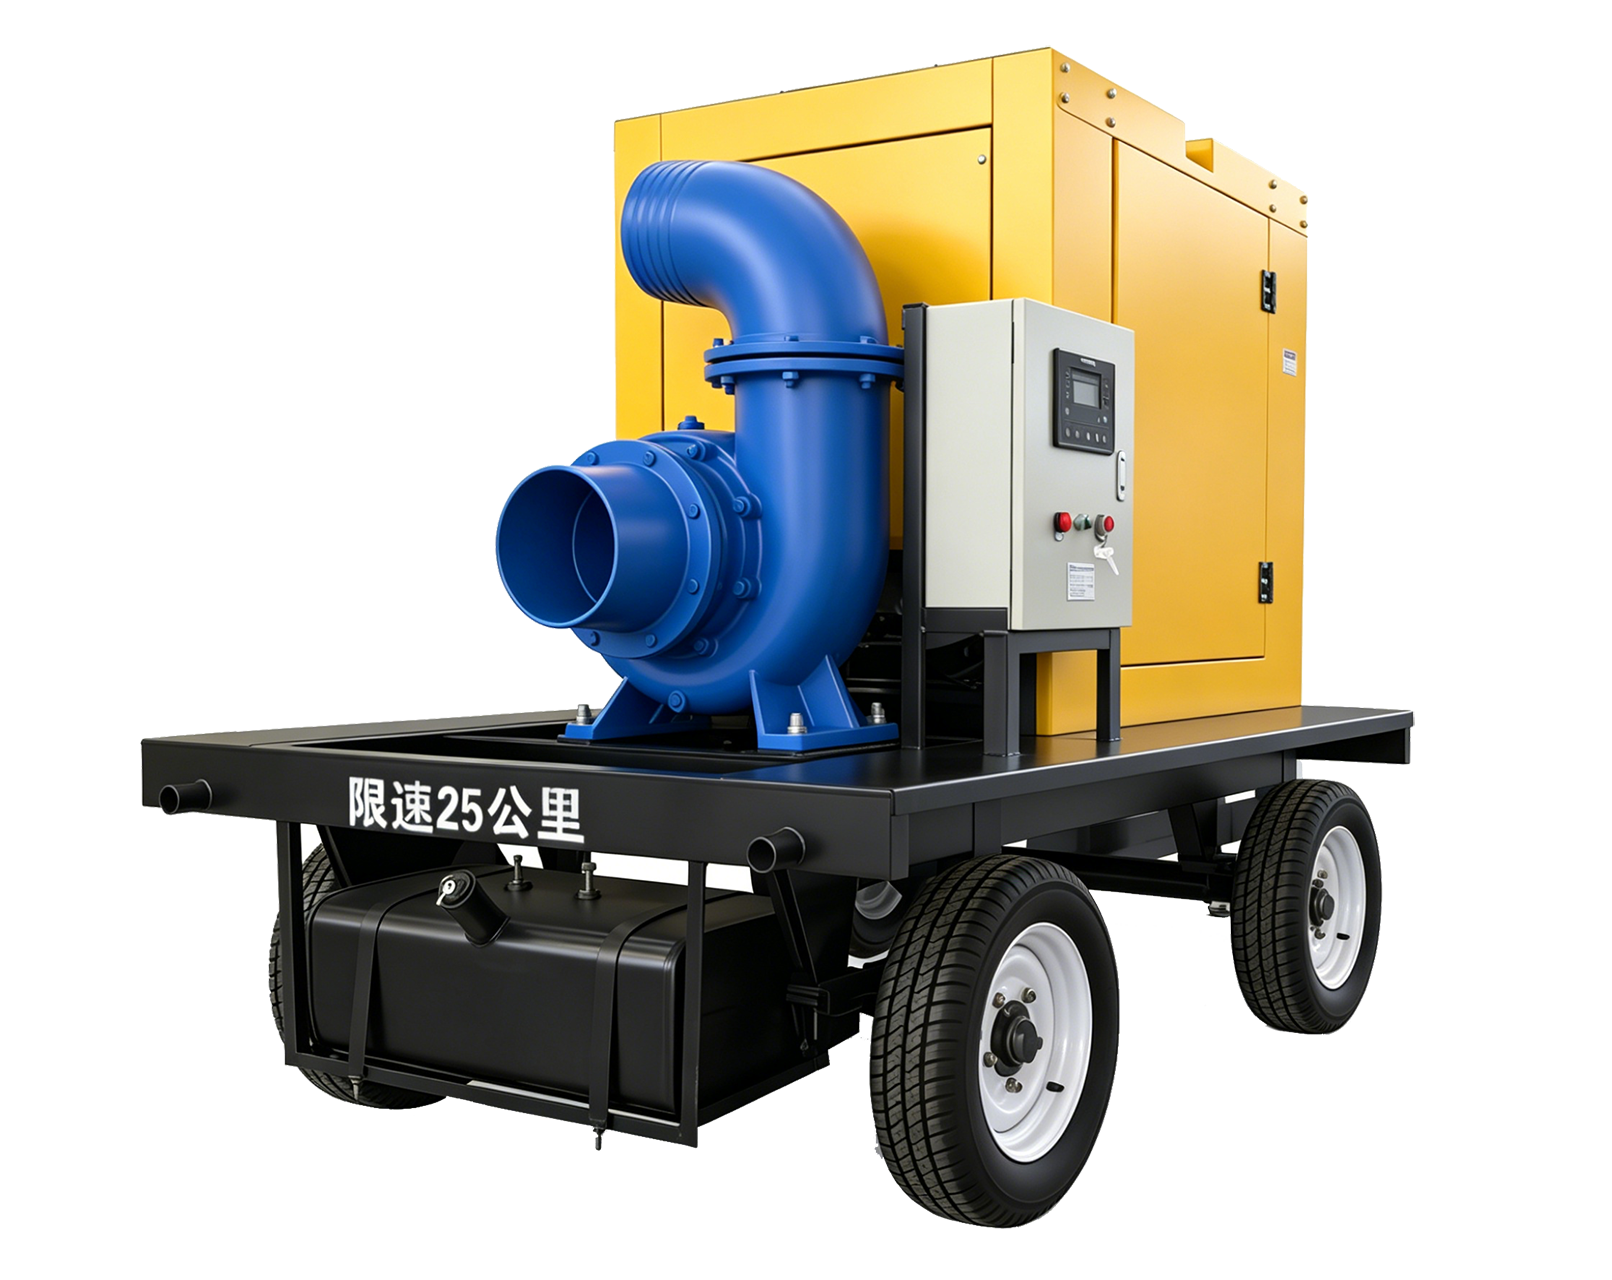
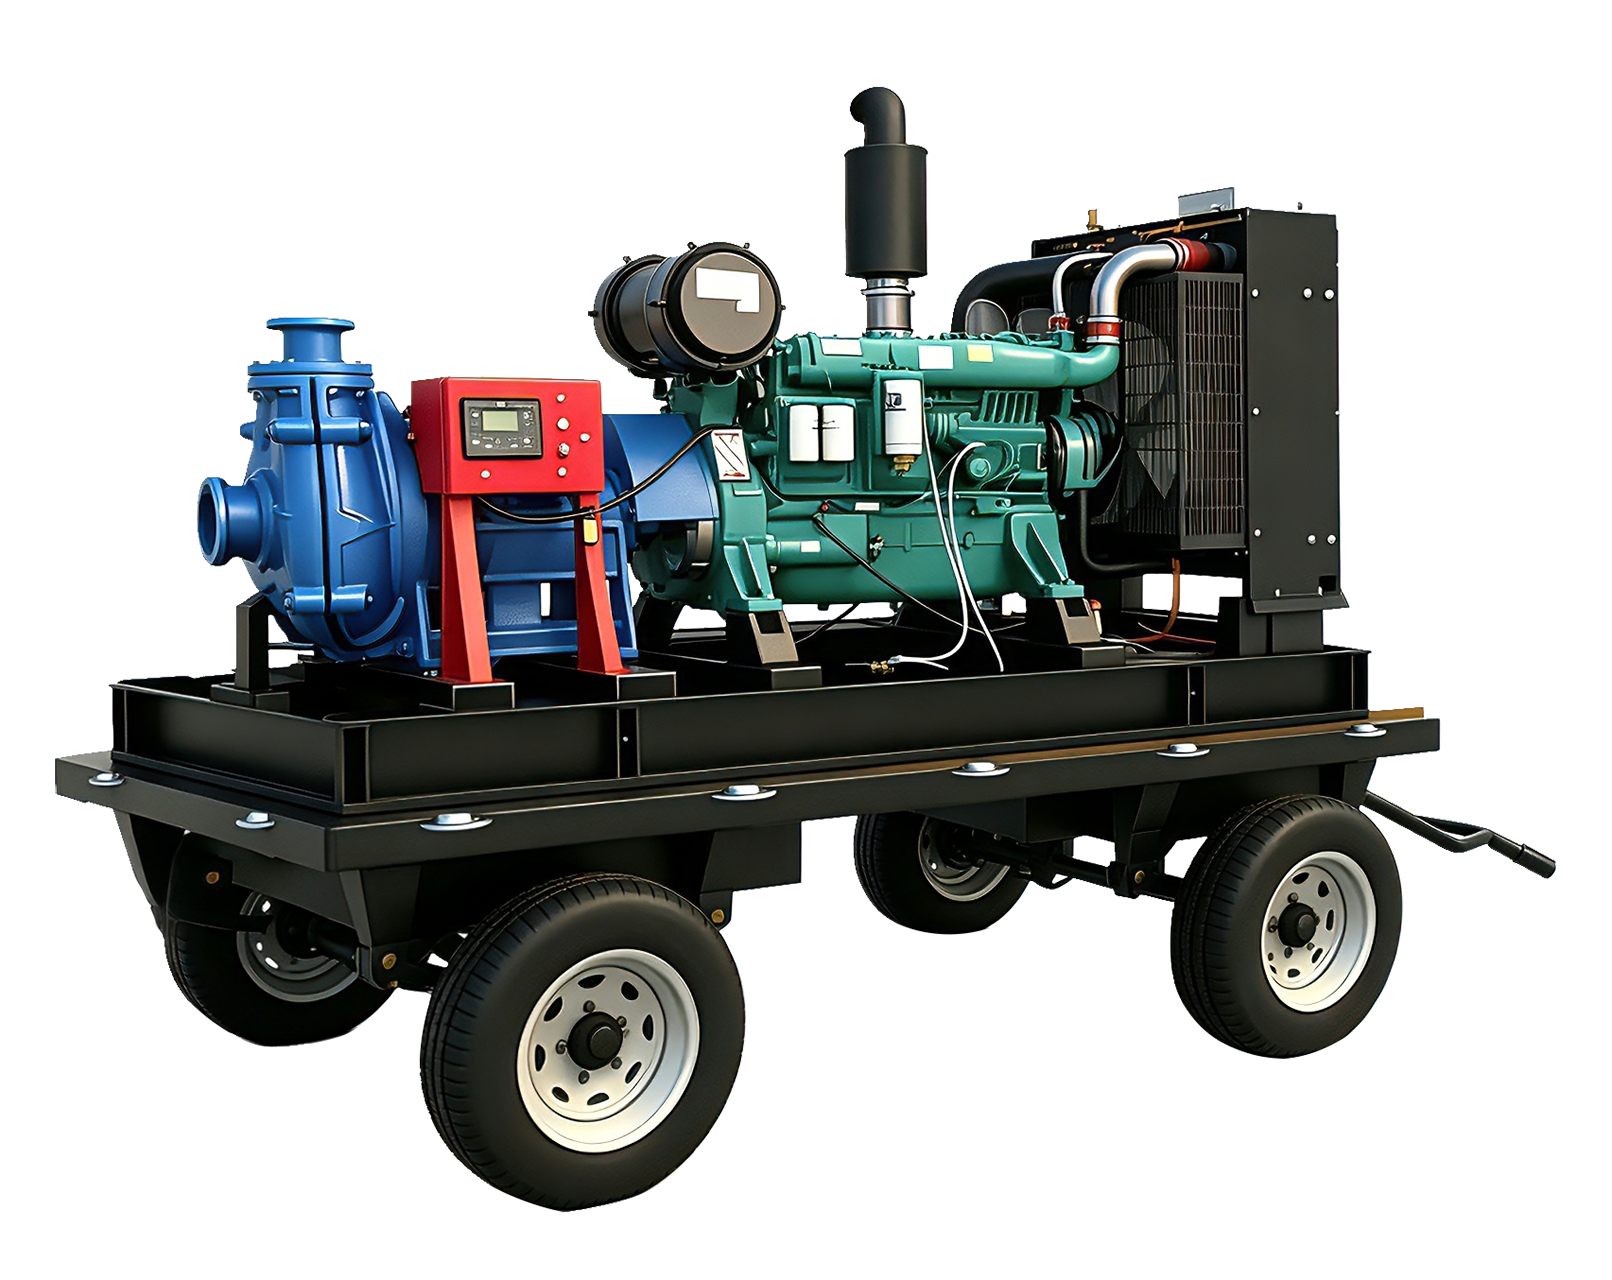
Diesel Pump
Diesel Pump
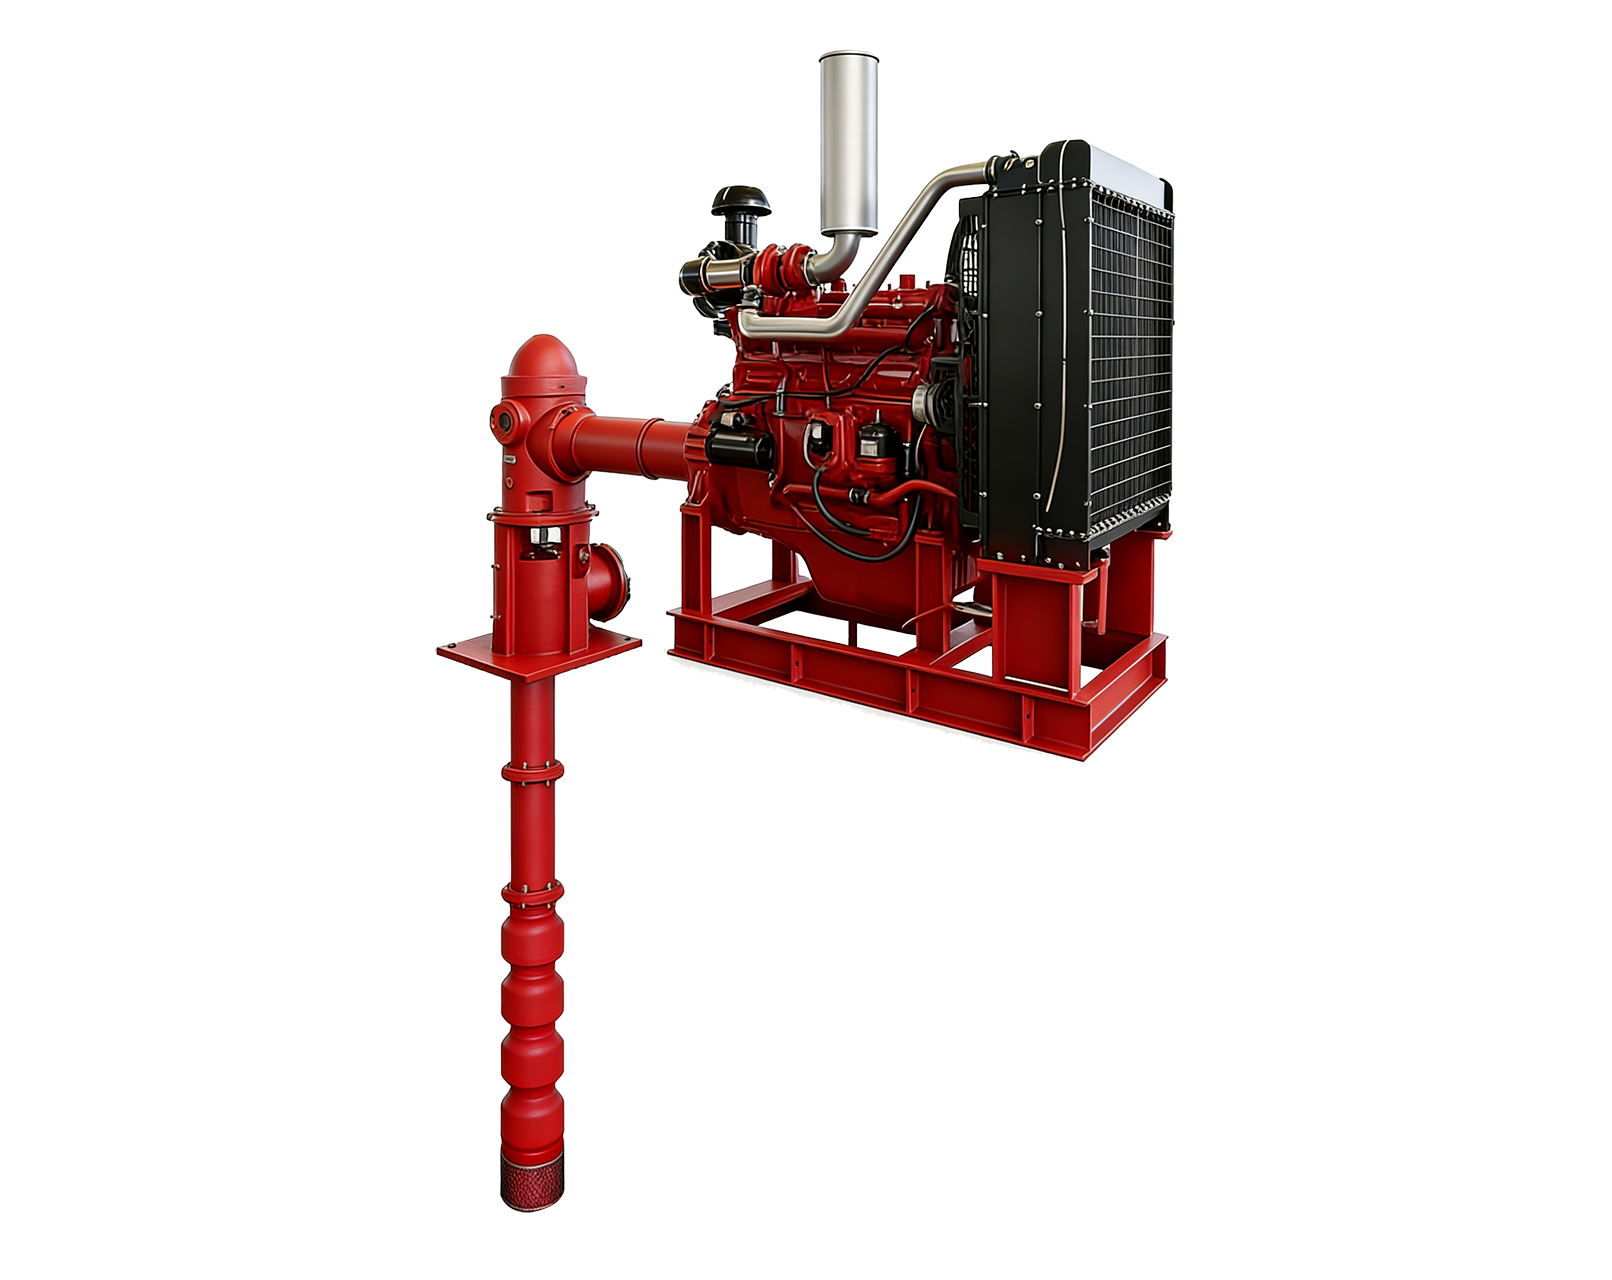
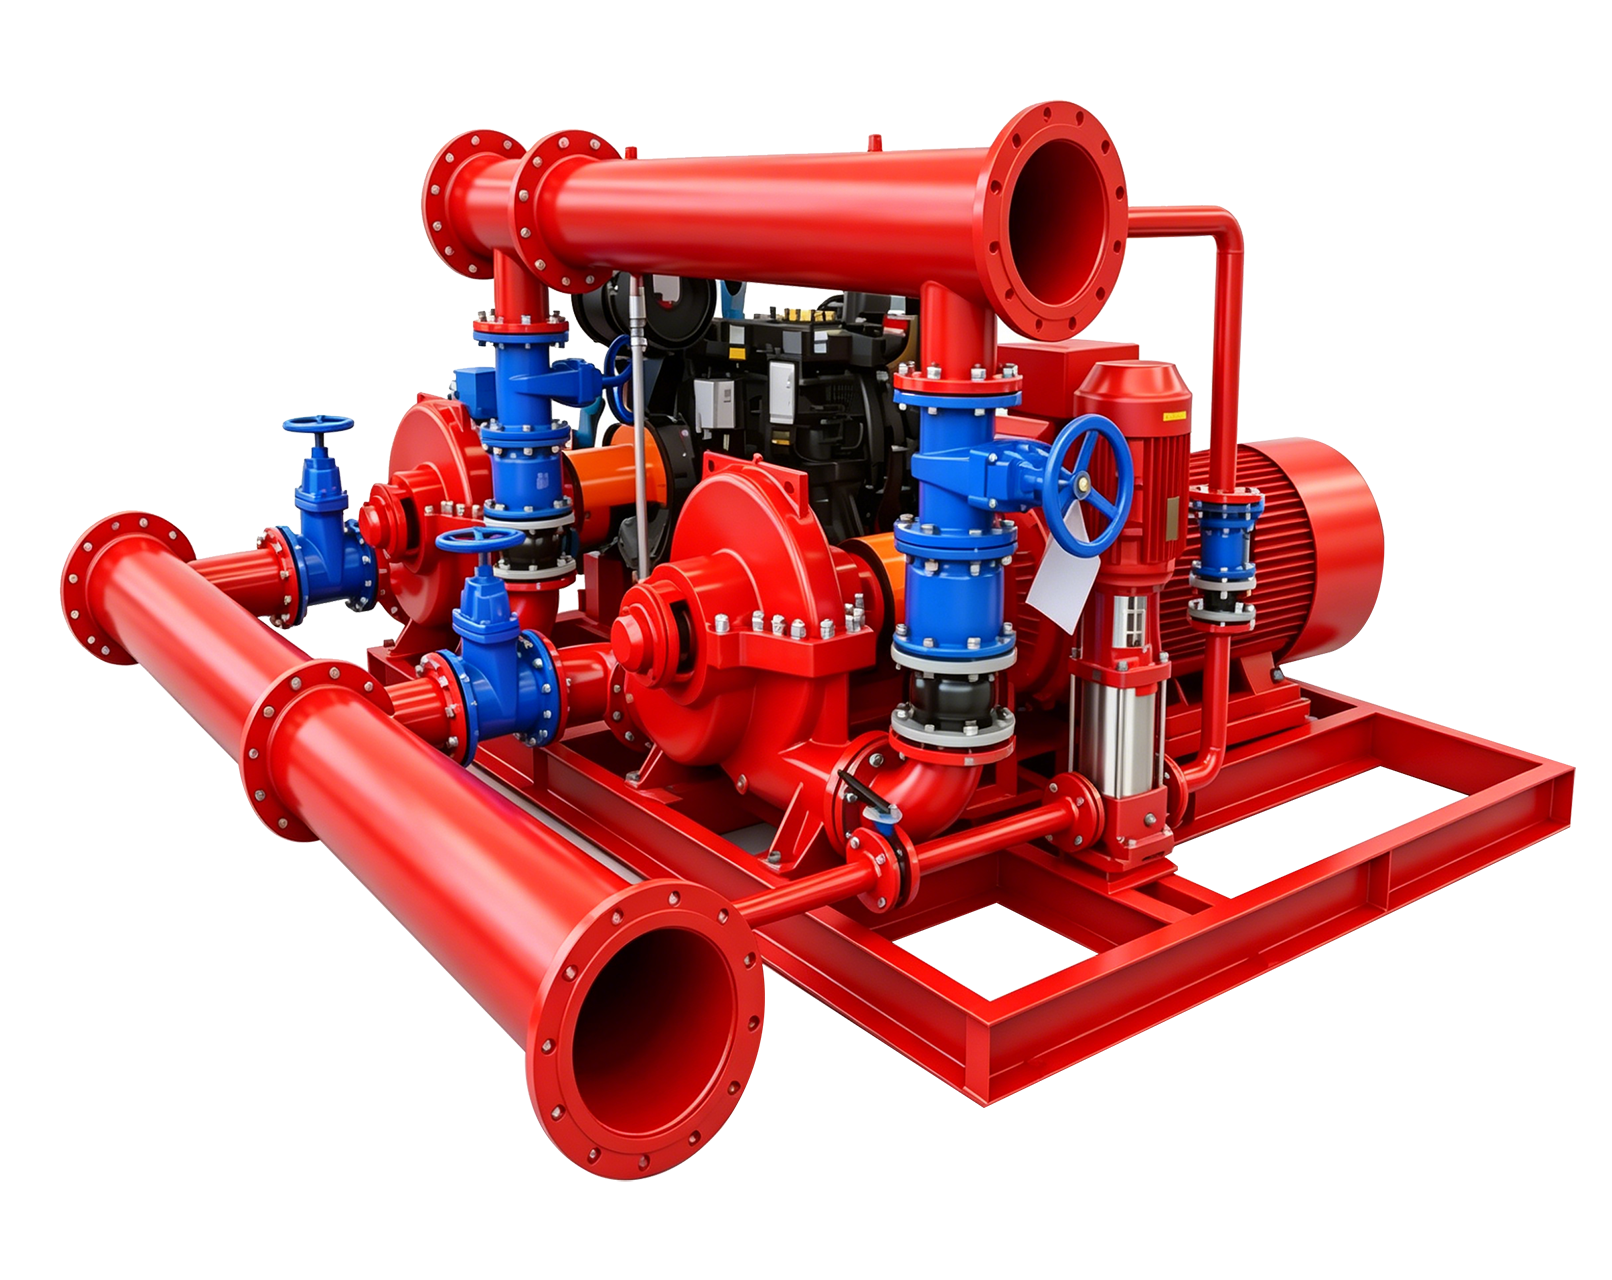
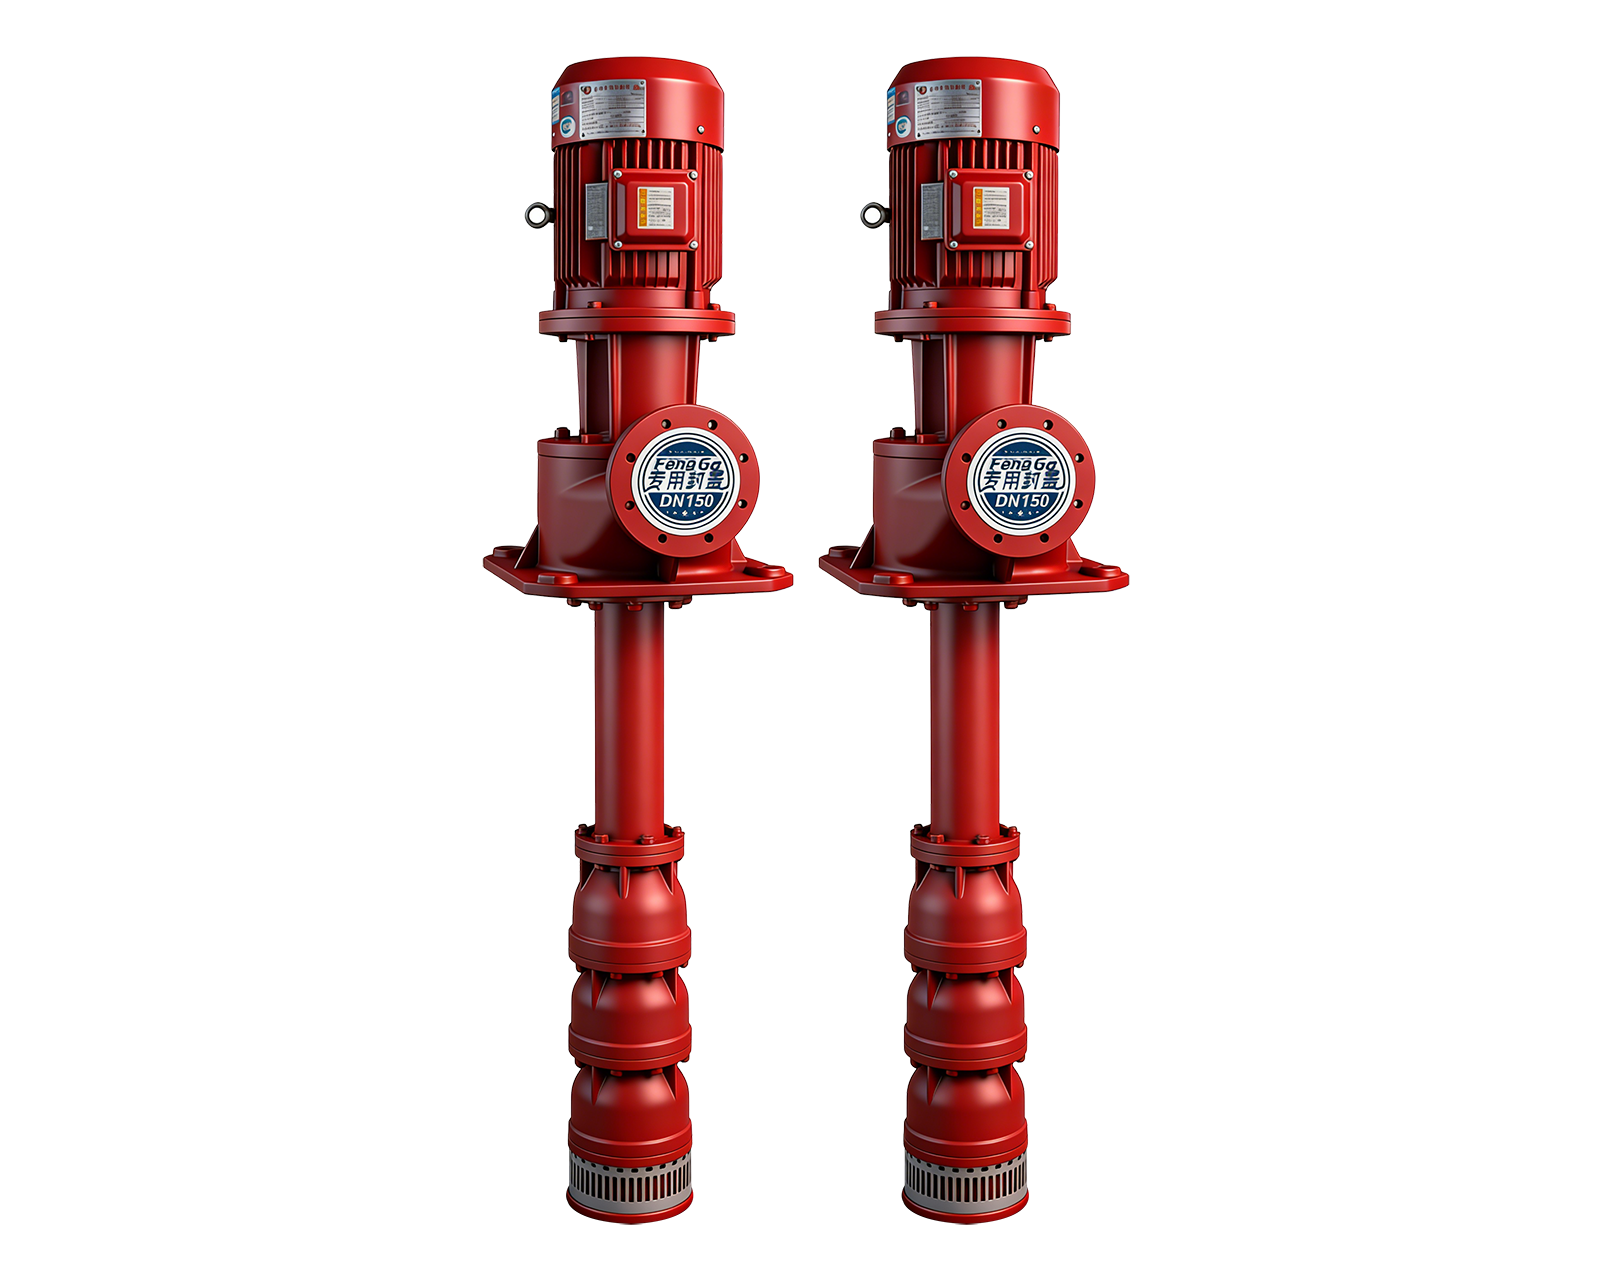
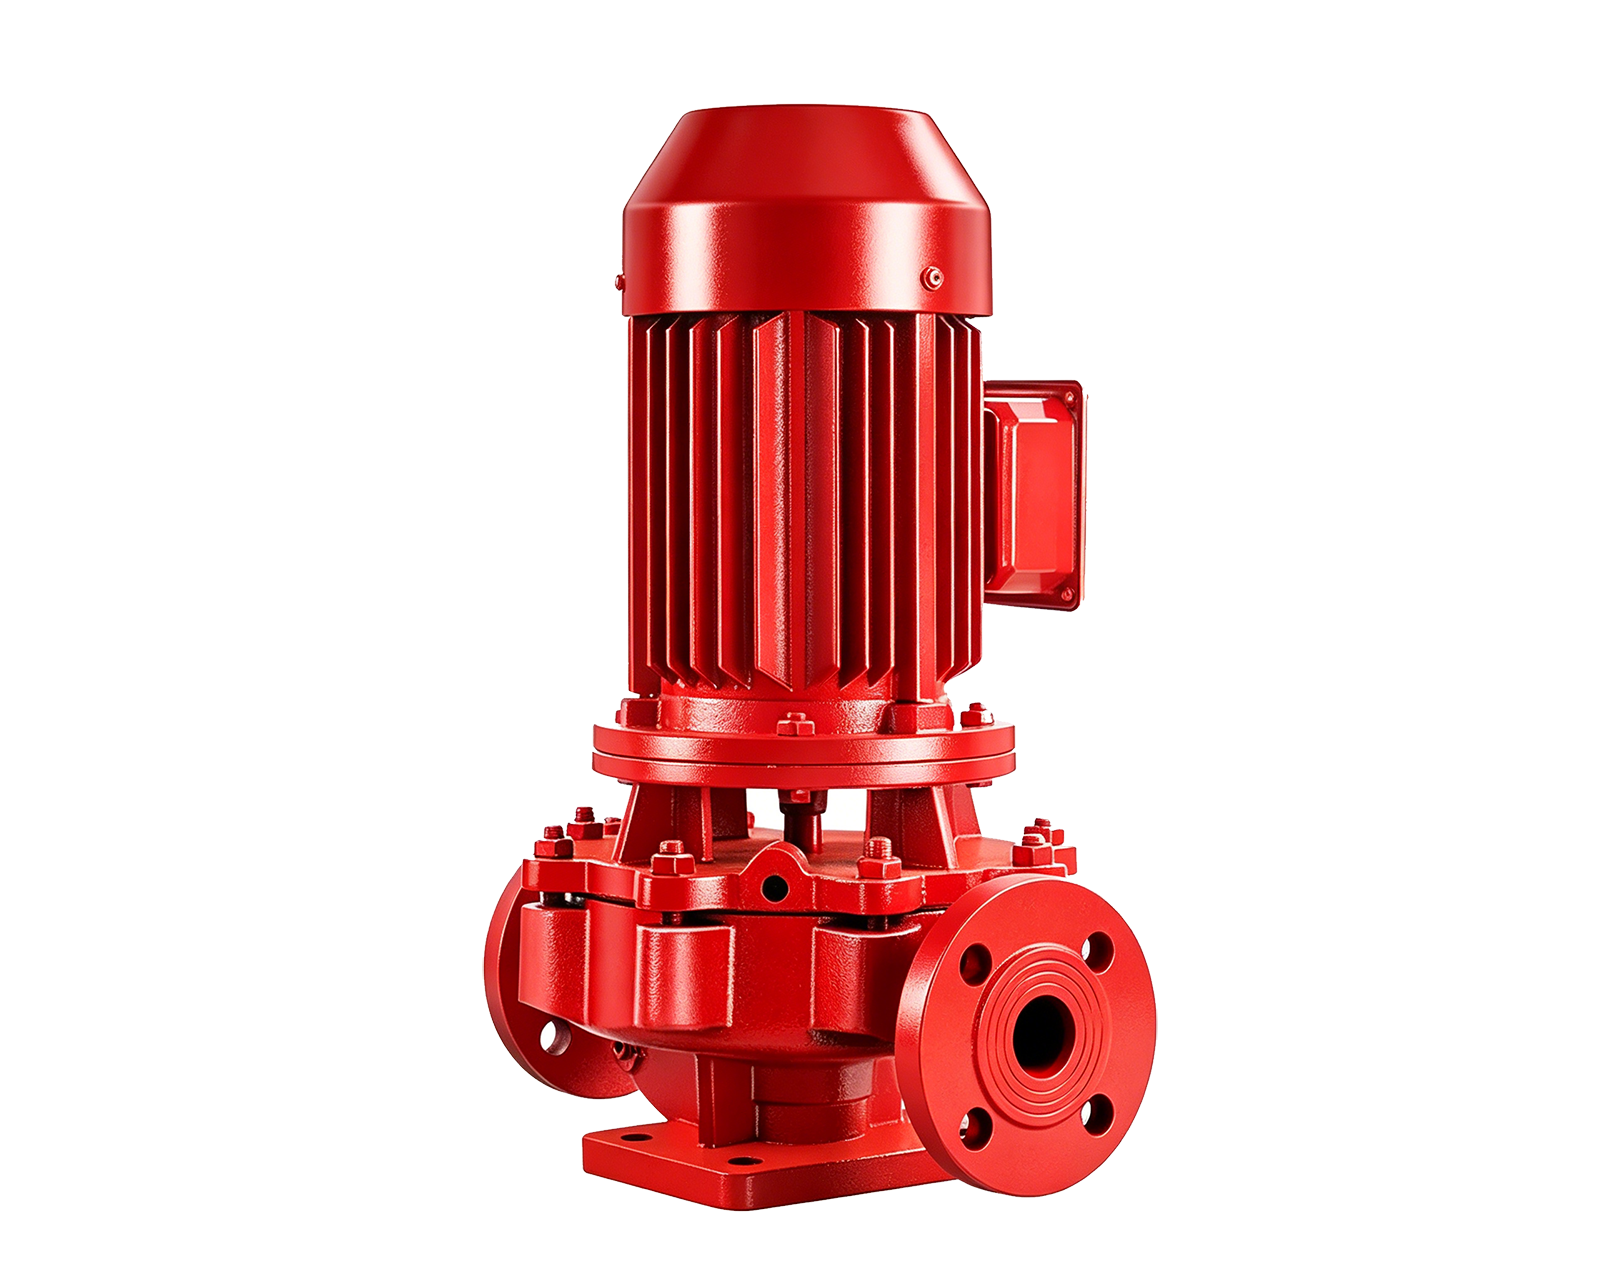
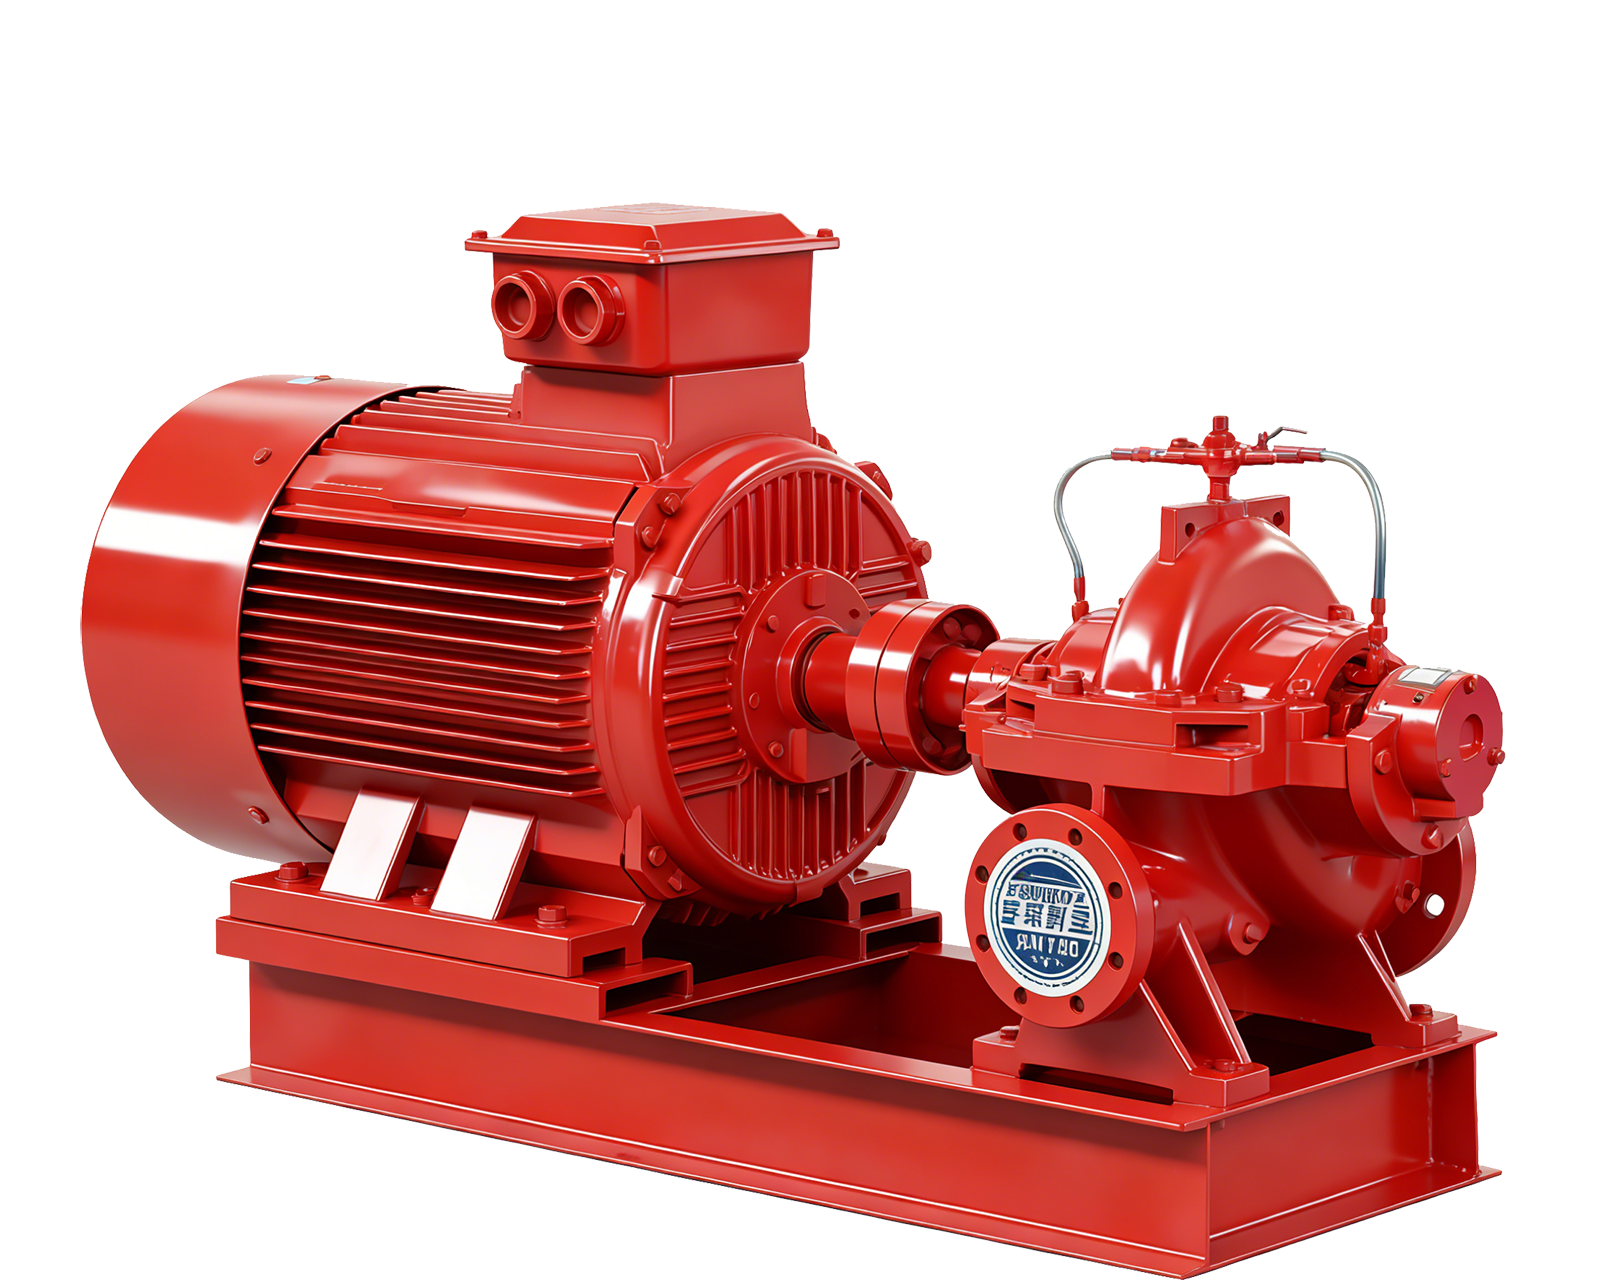
Fire Pump
Fire Pump
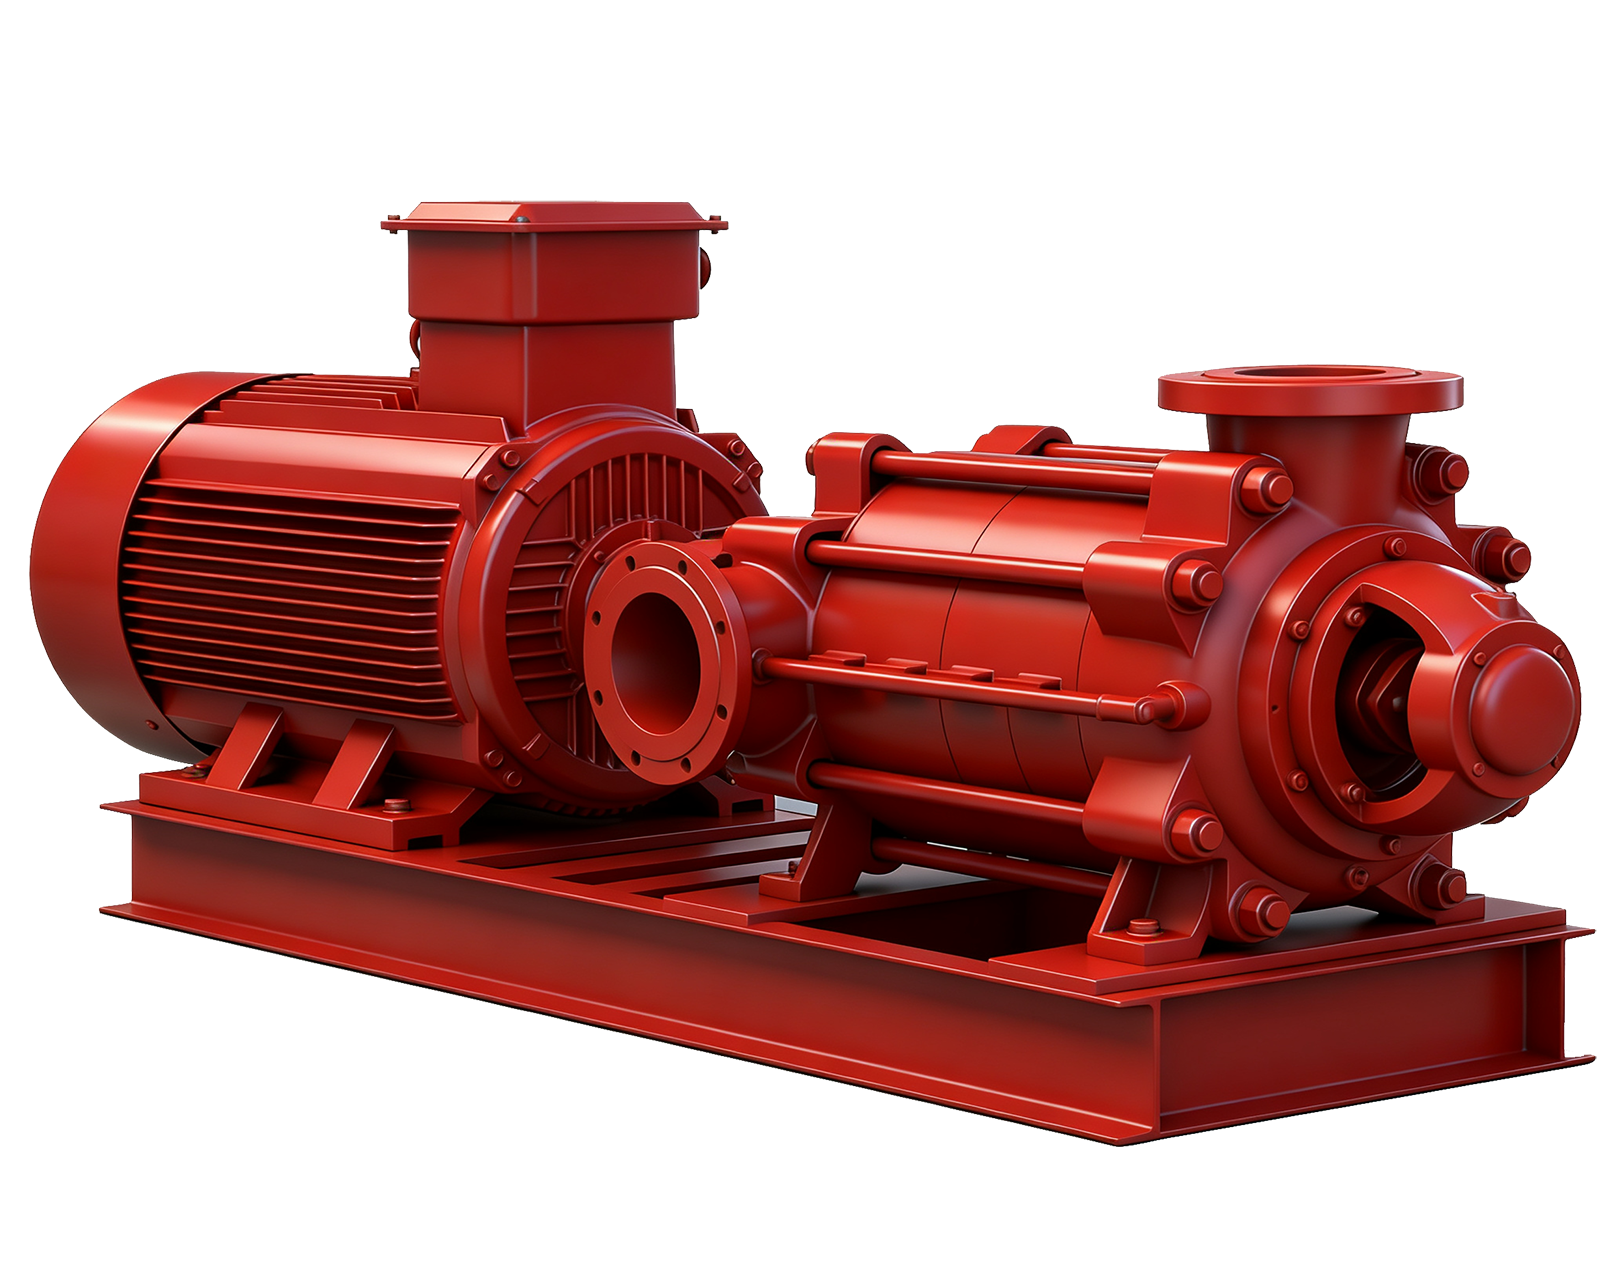
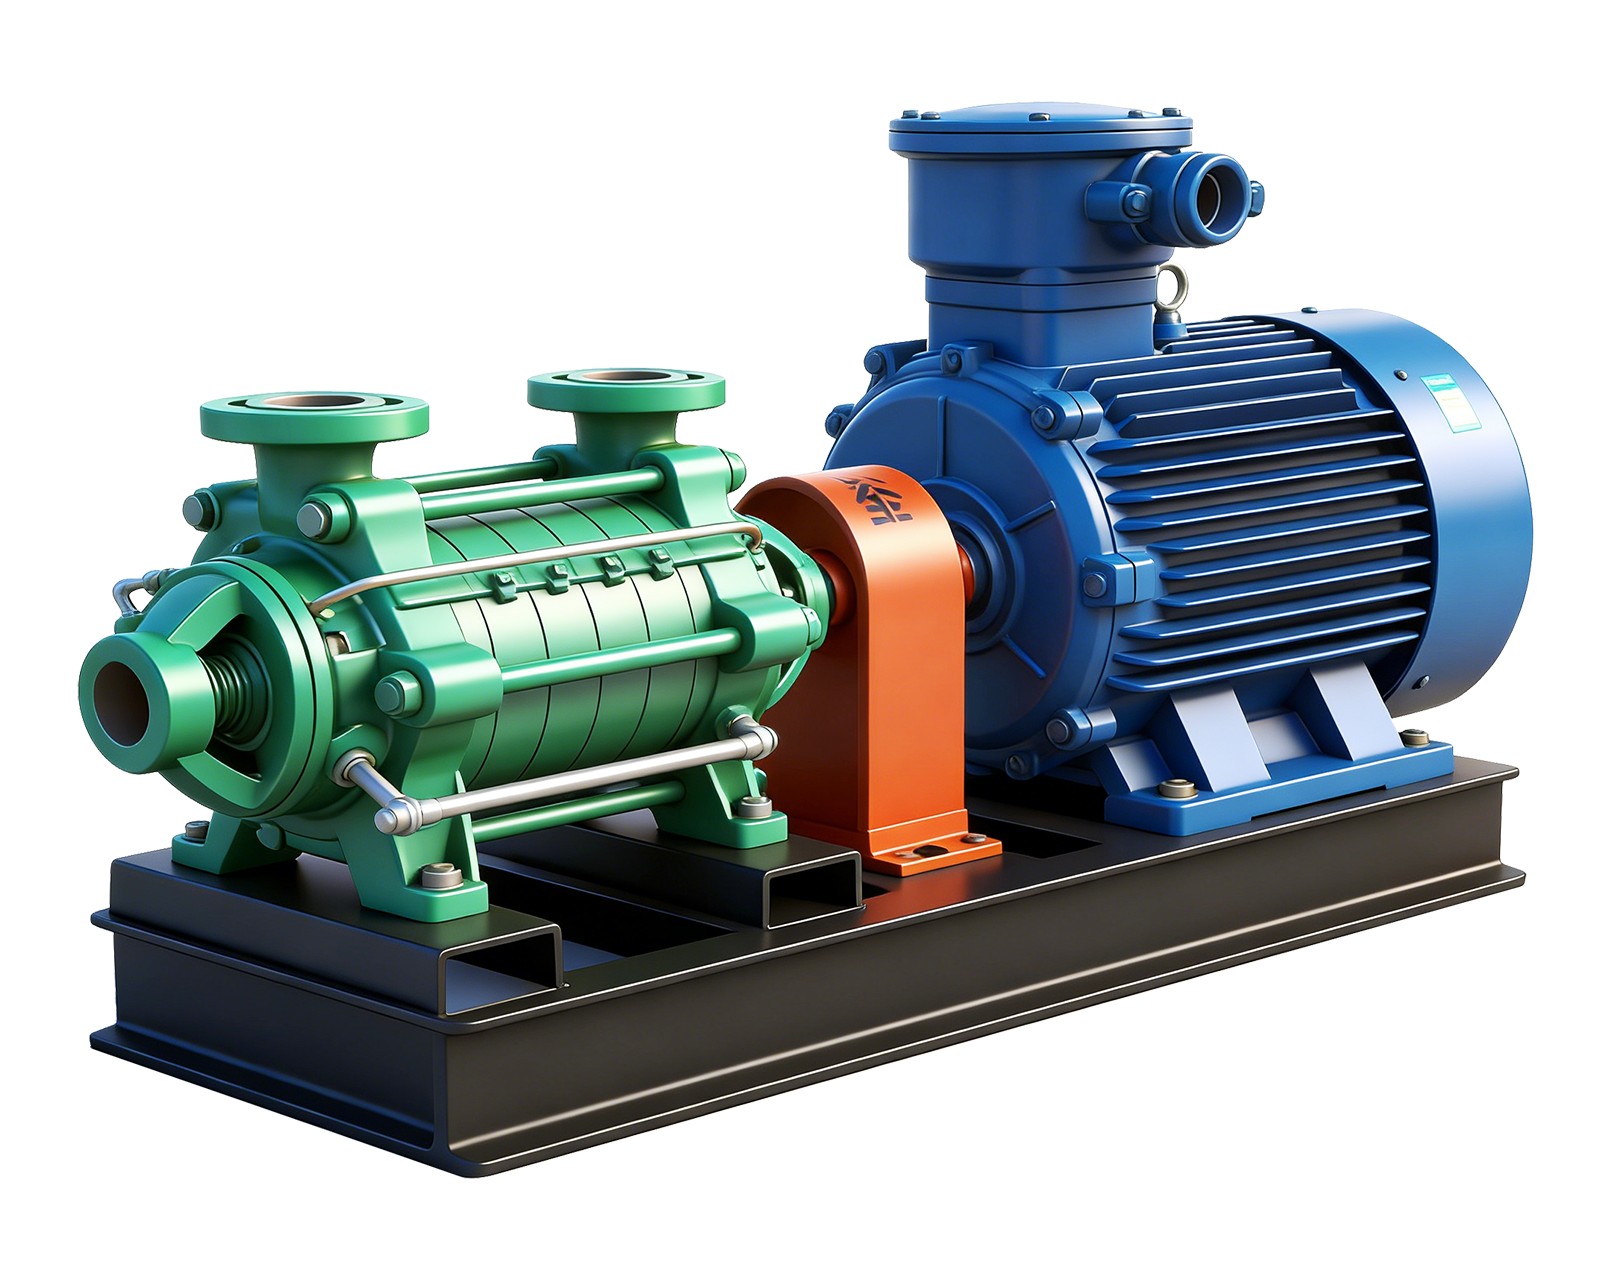
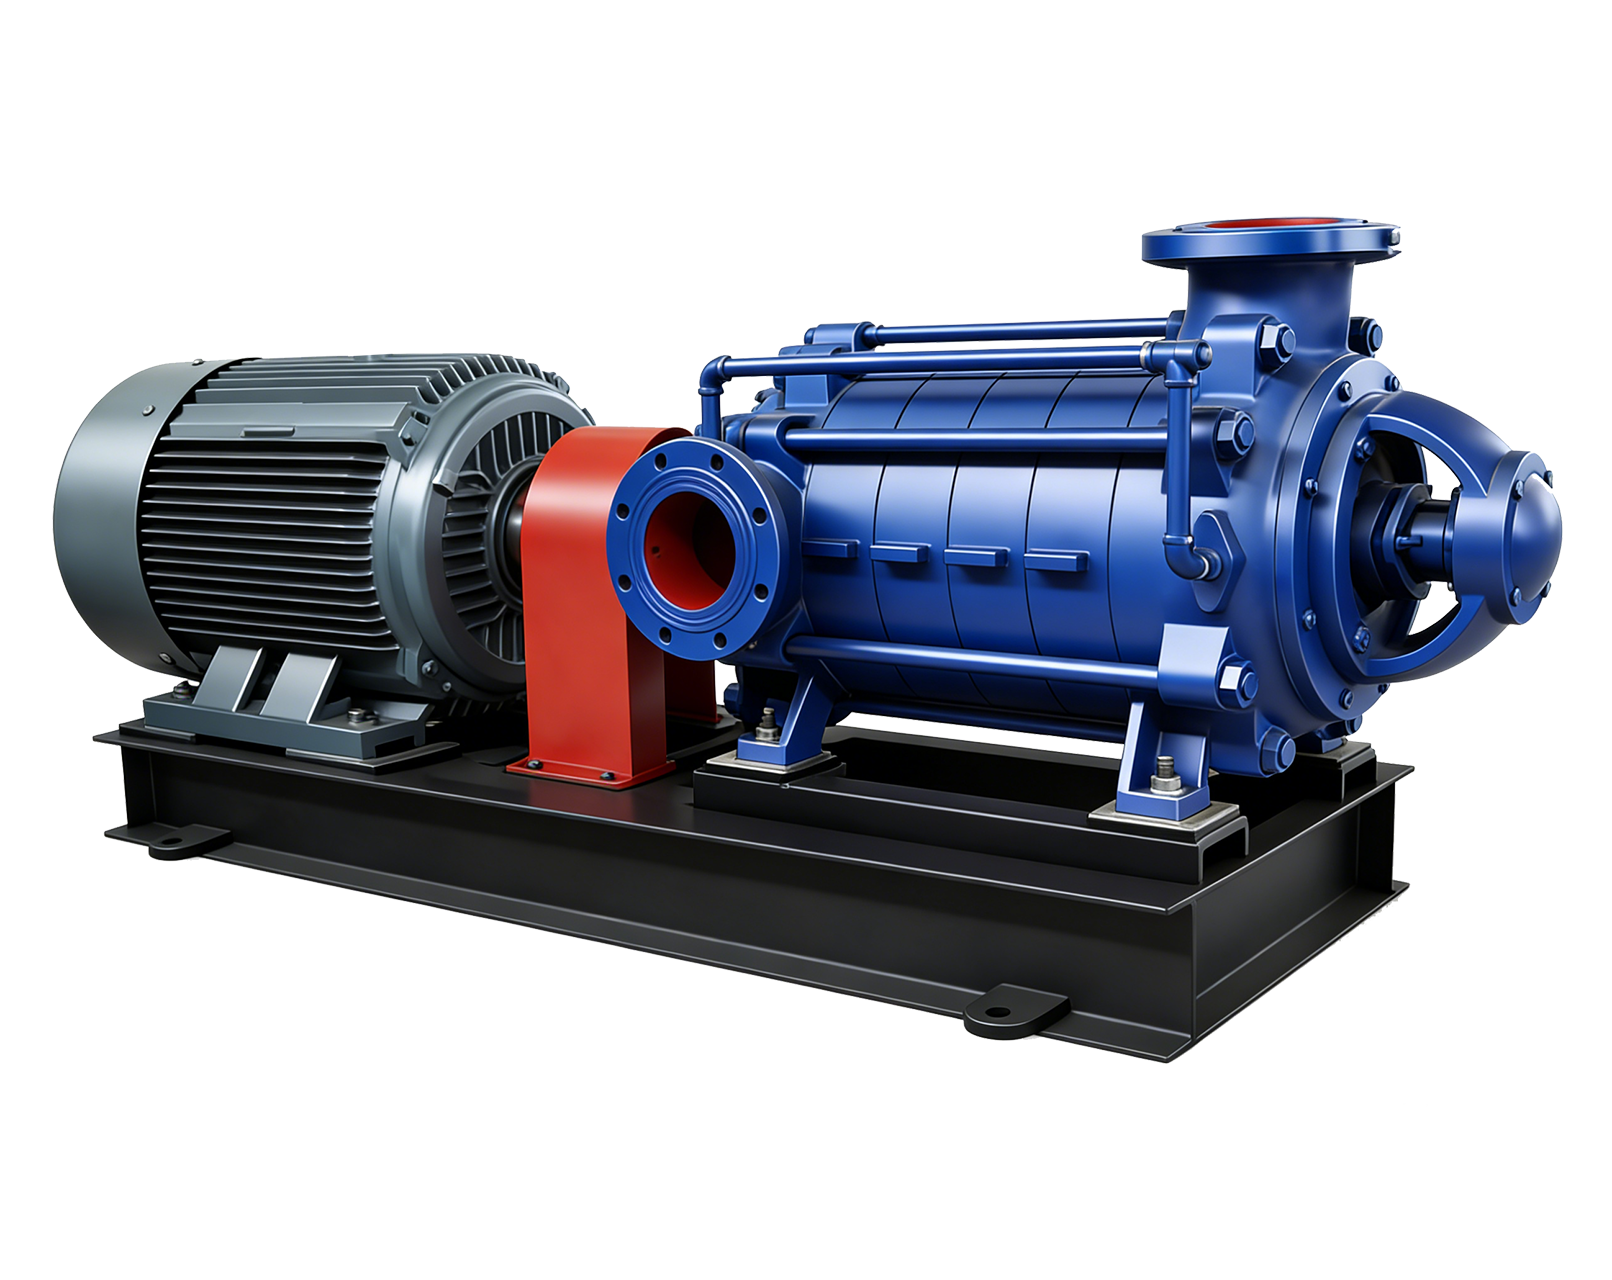
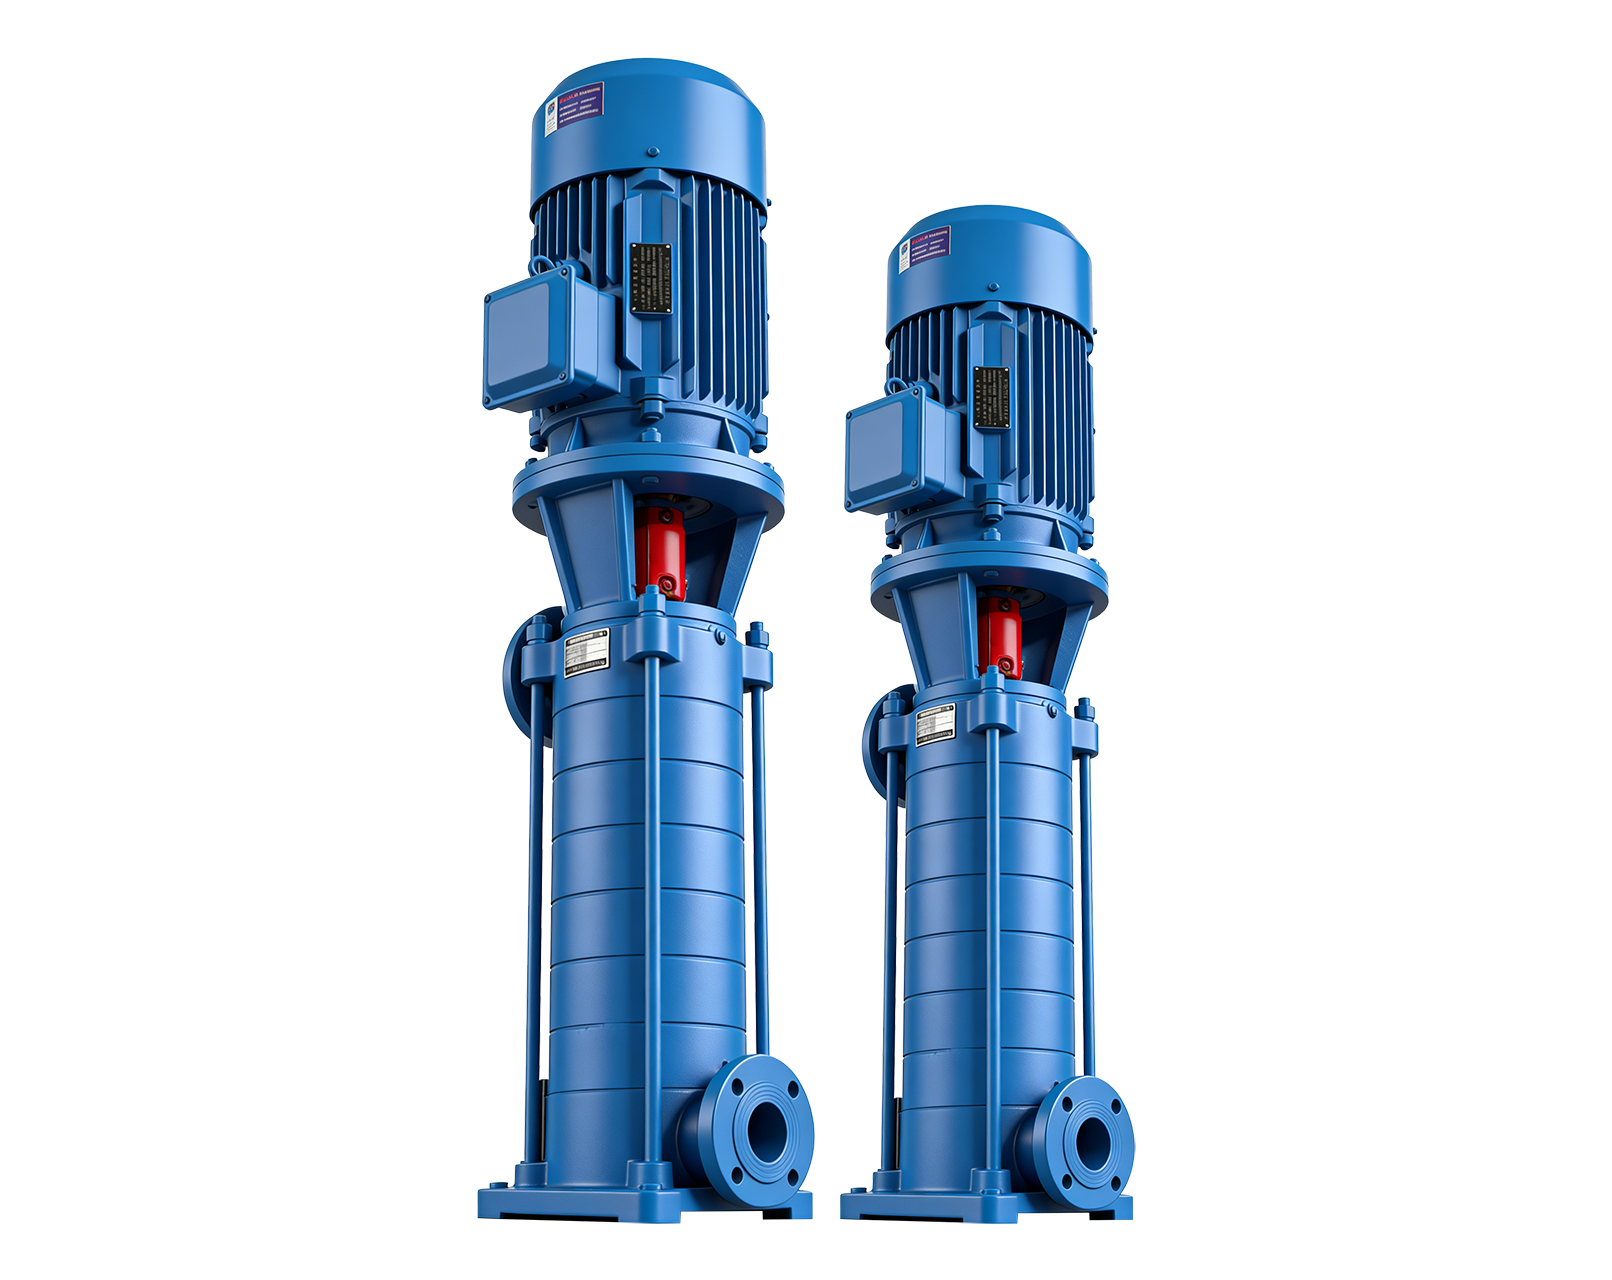
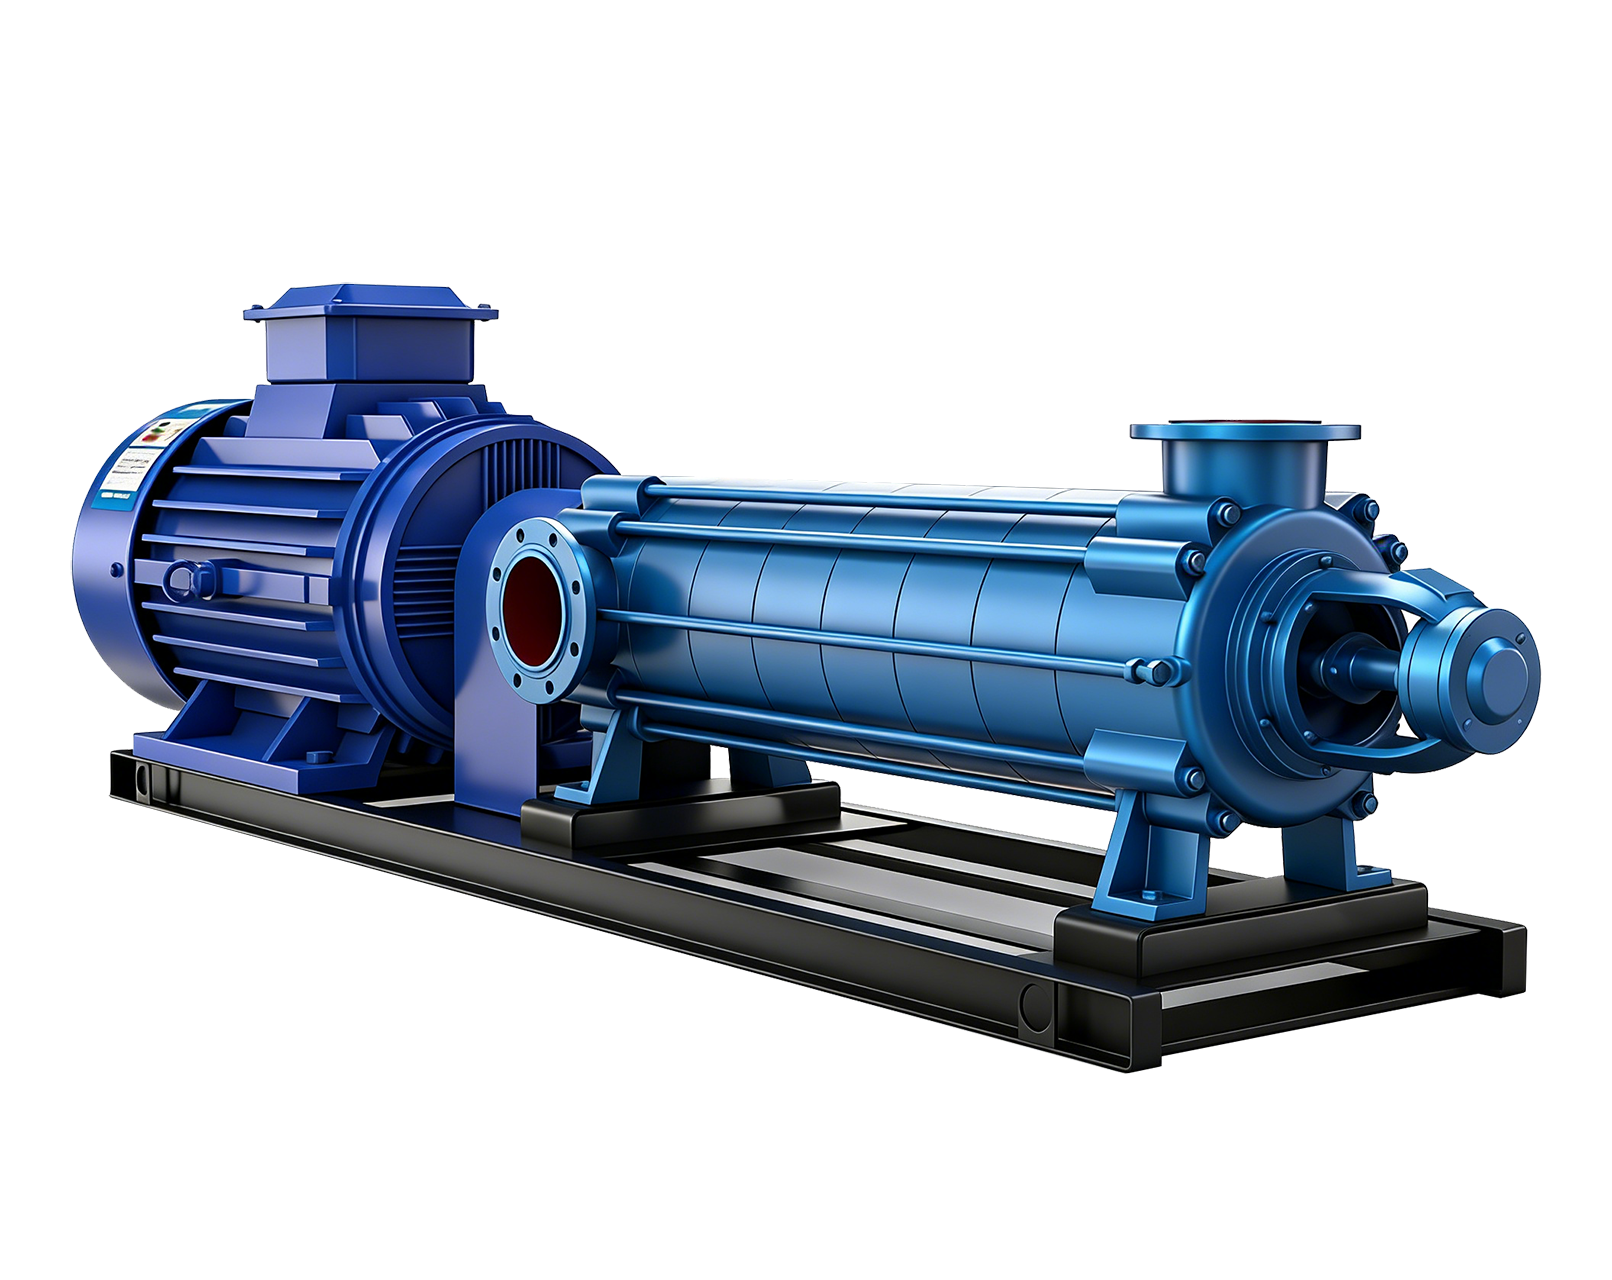
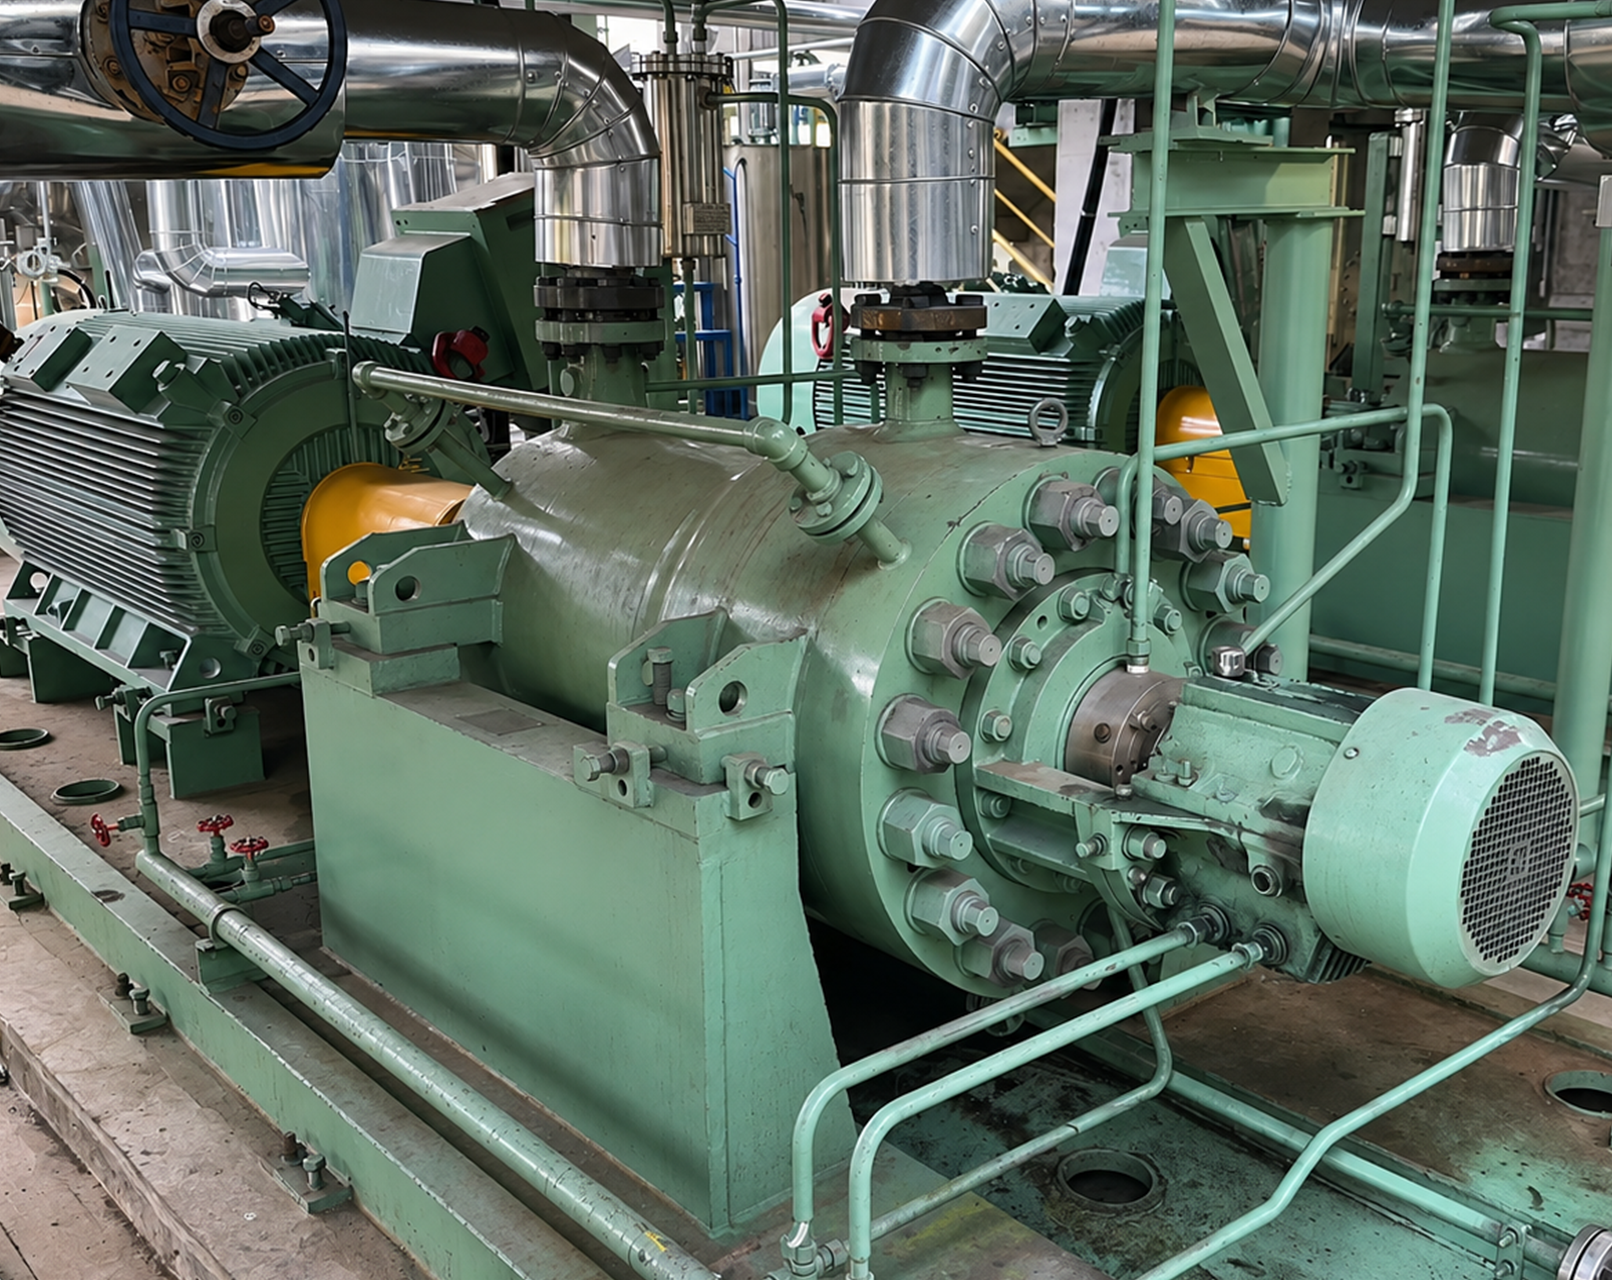
Multistage Pump
Multistage Pump
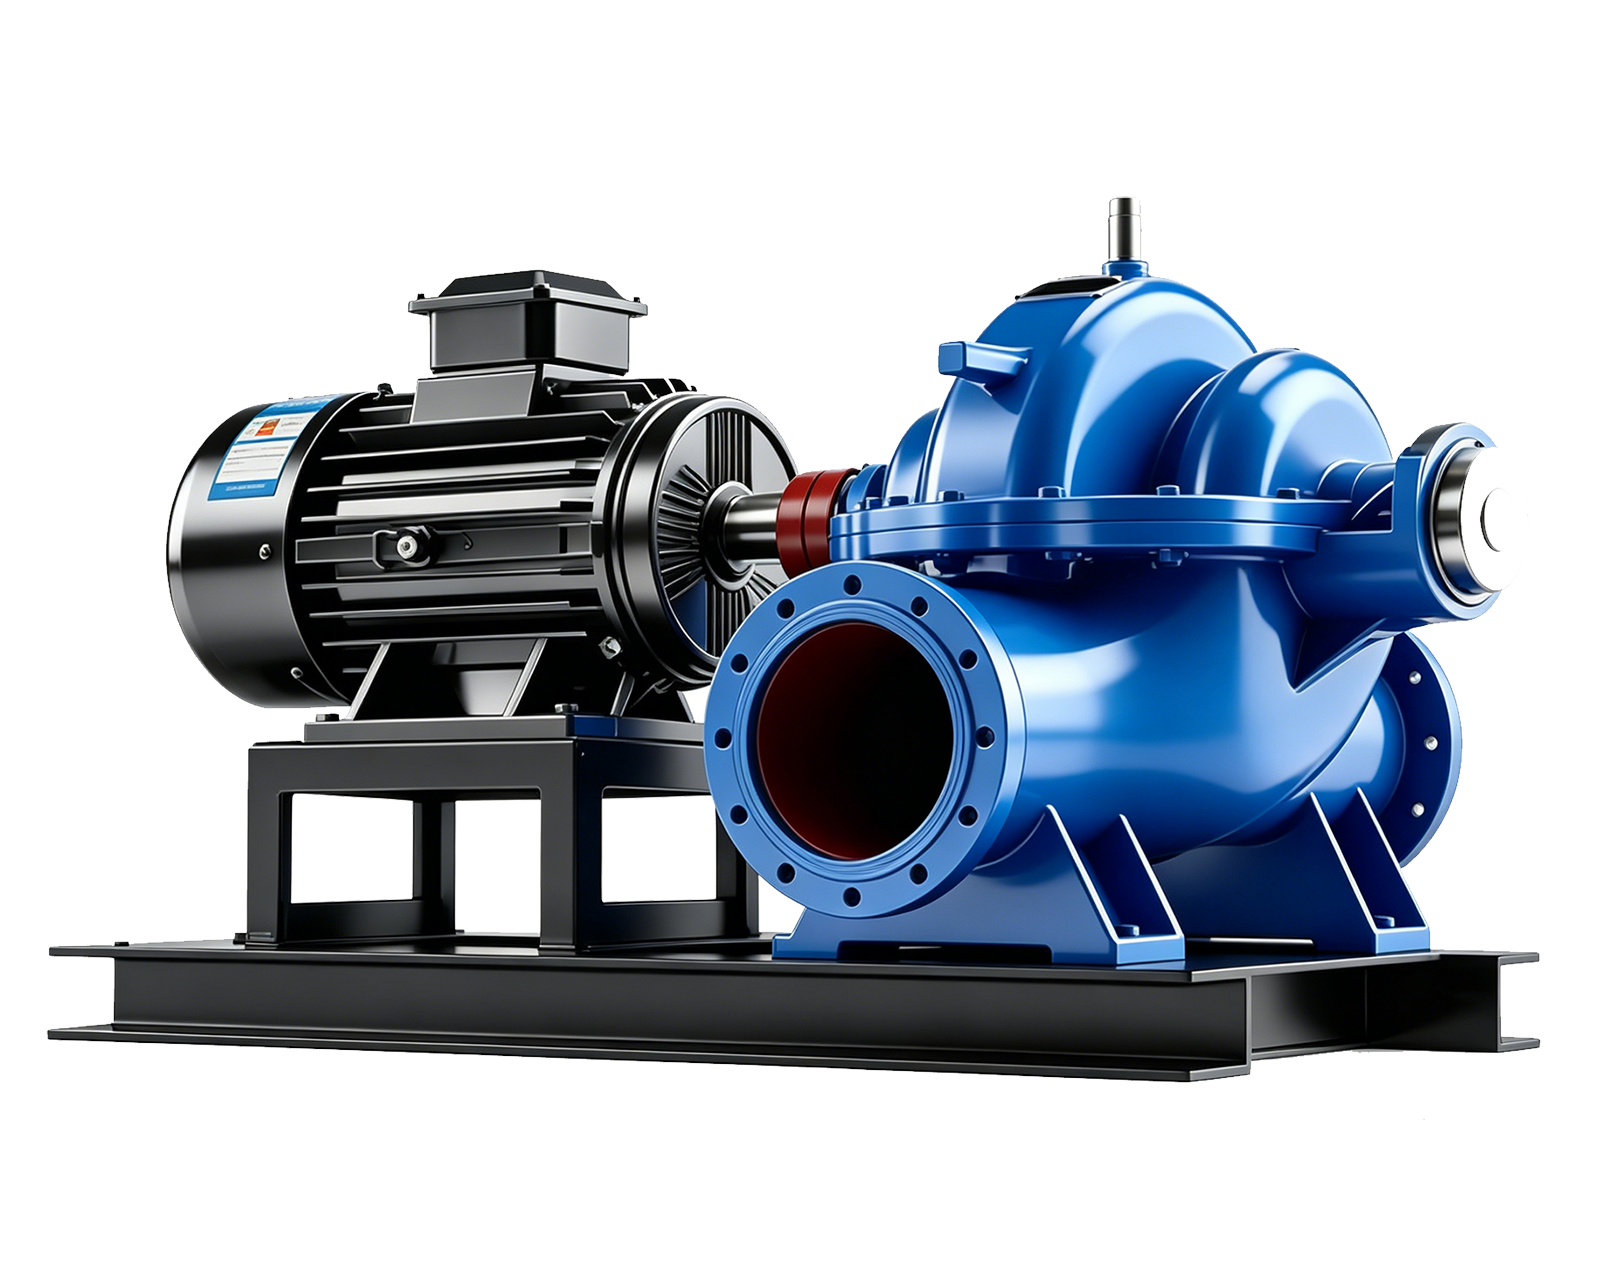
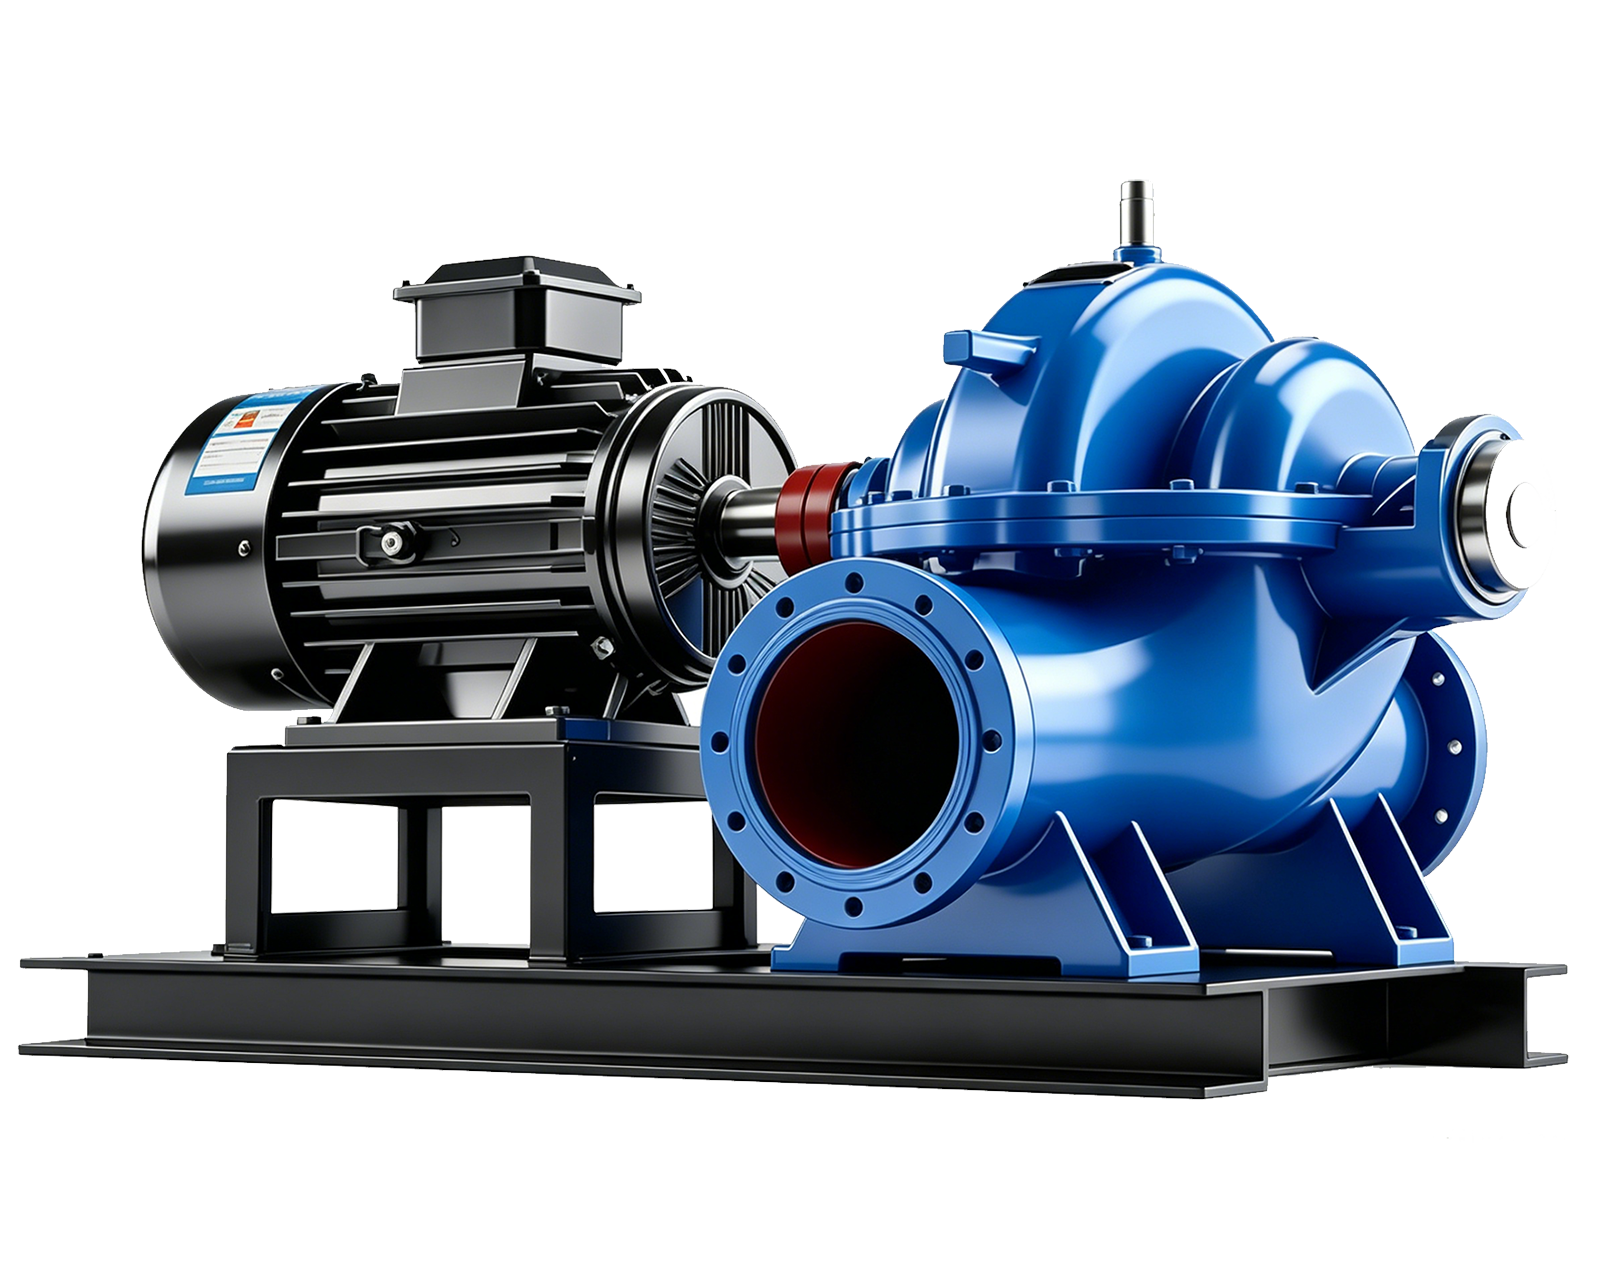
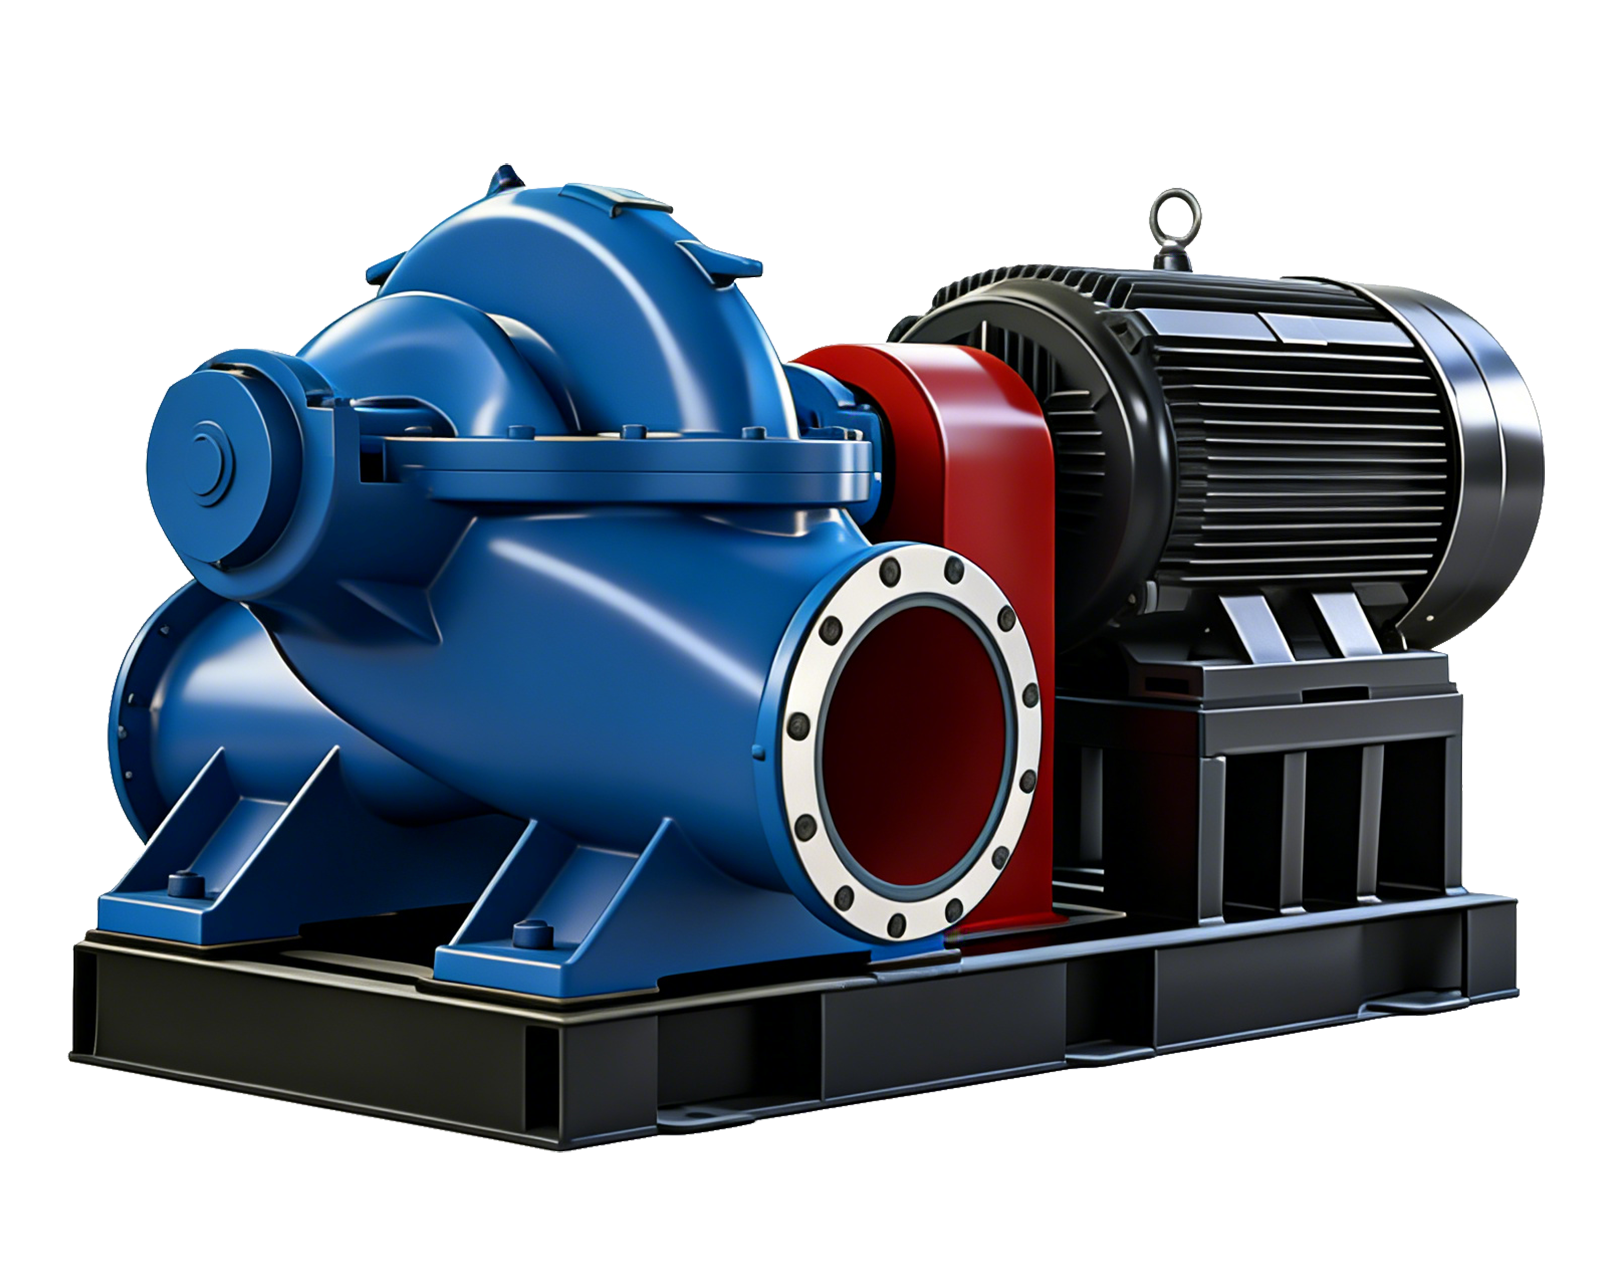
Split Case Pump
Split Case Pump
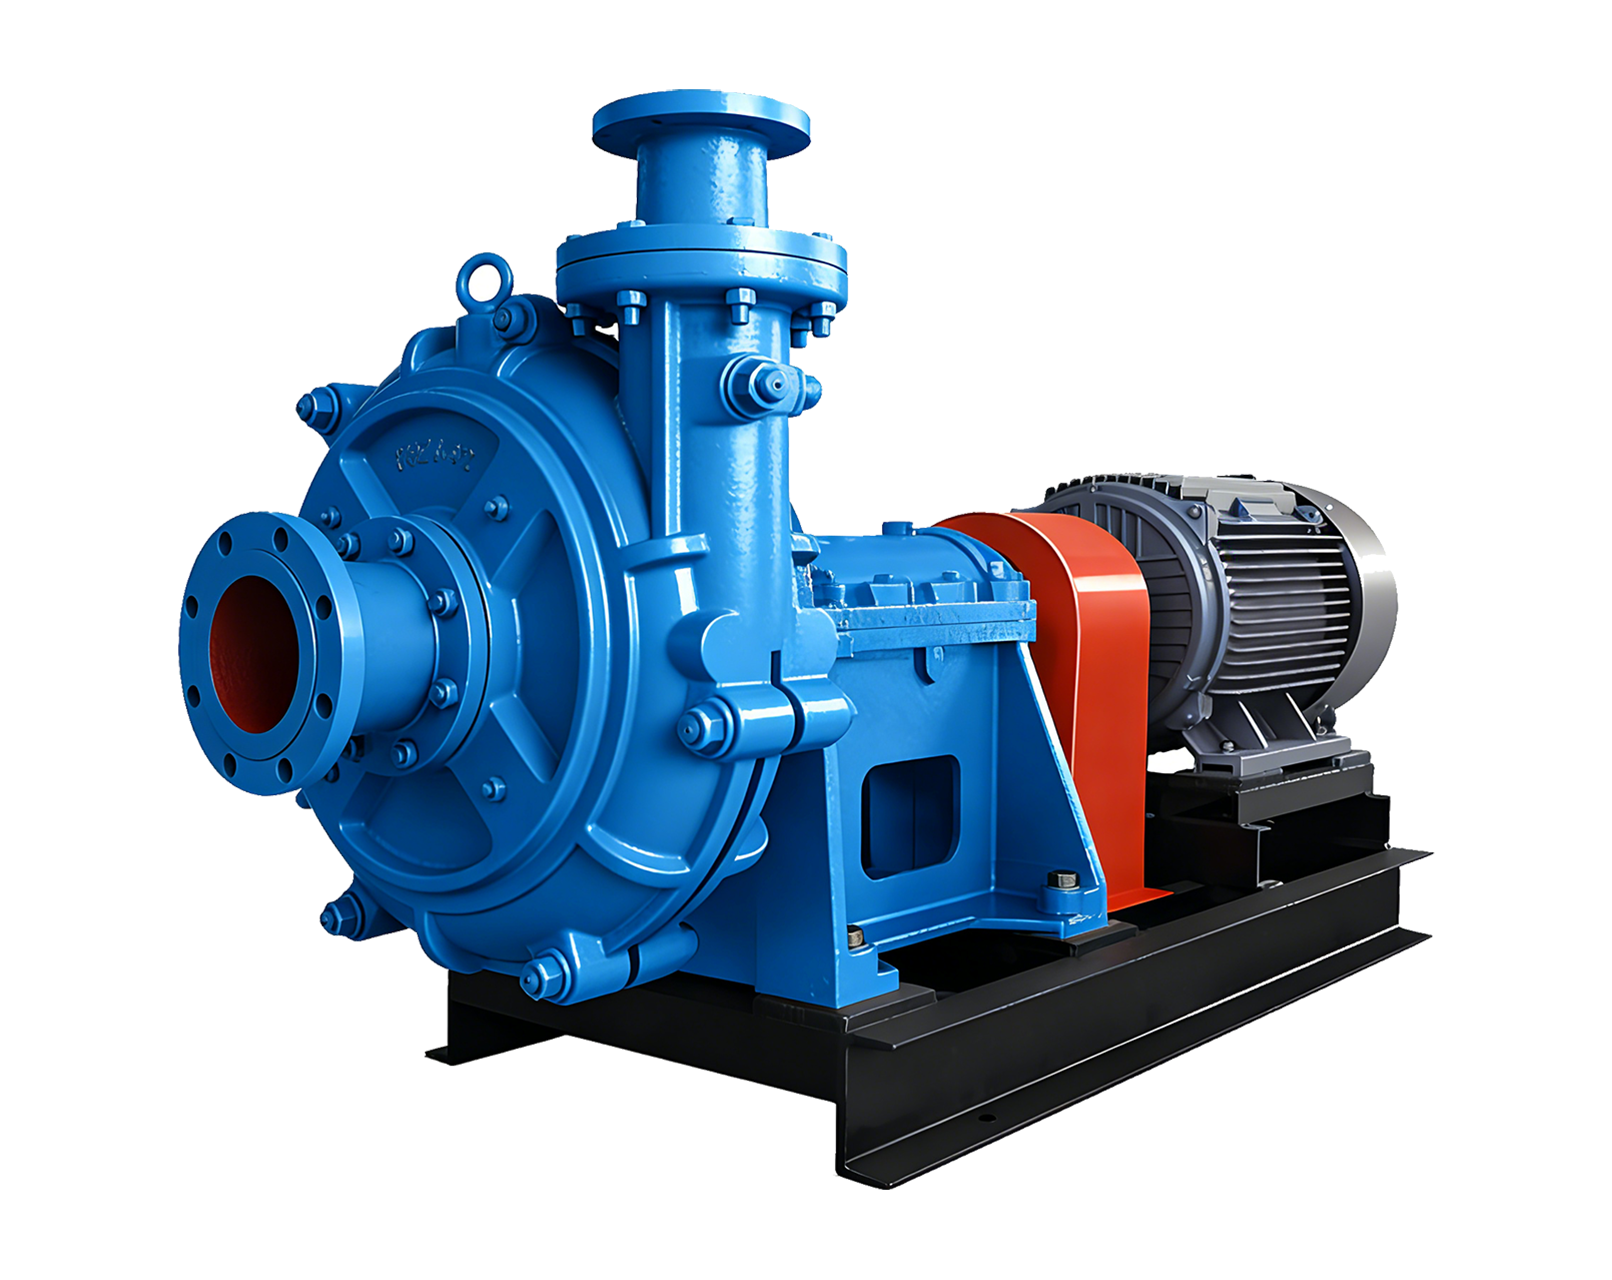
Slurry Pump
Slurry Pump
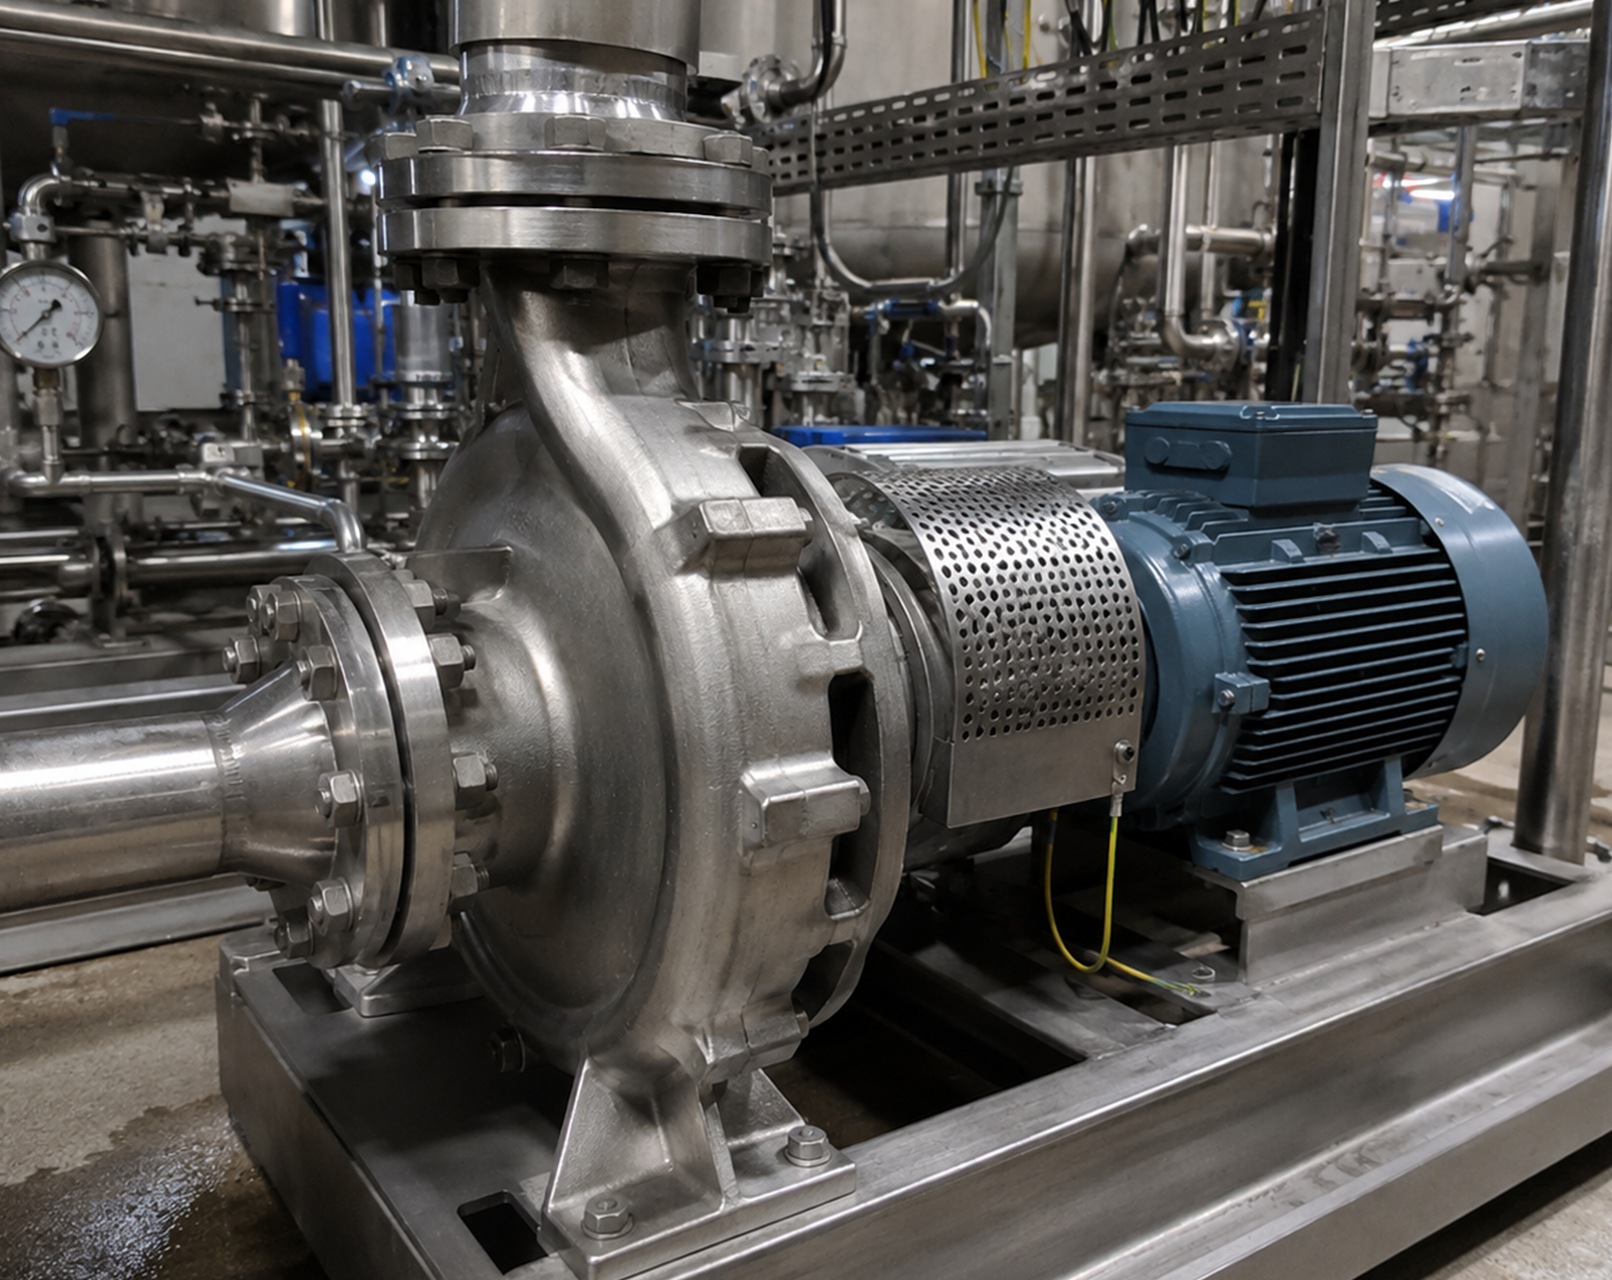
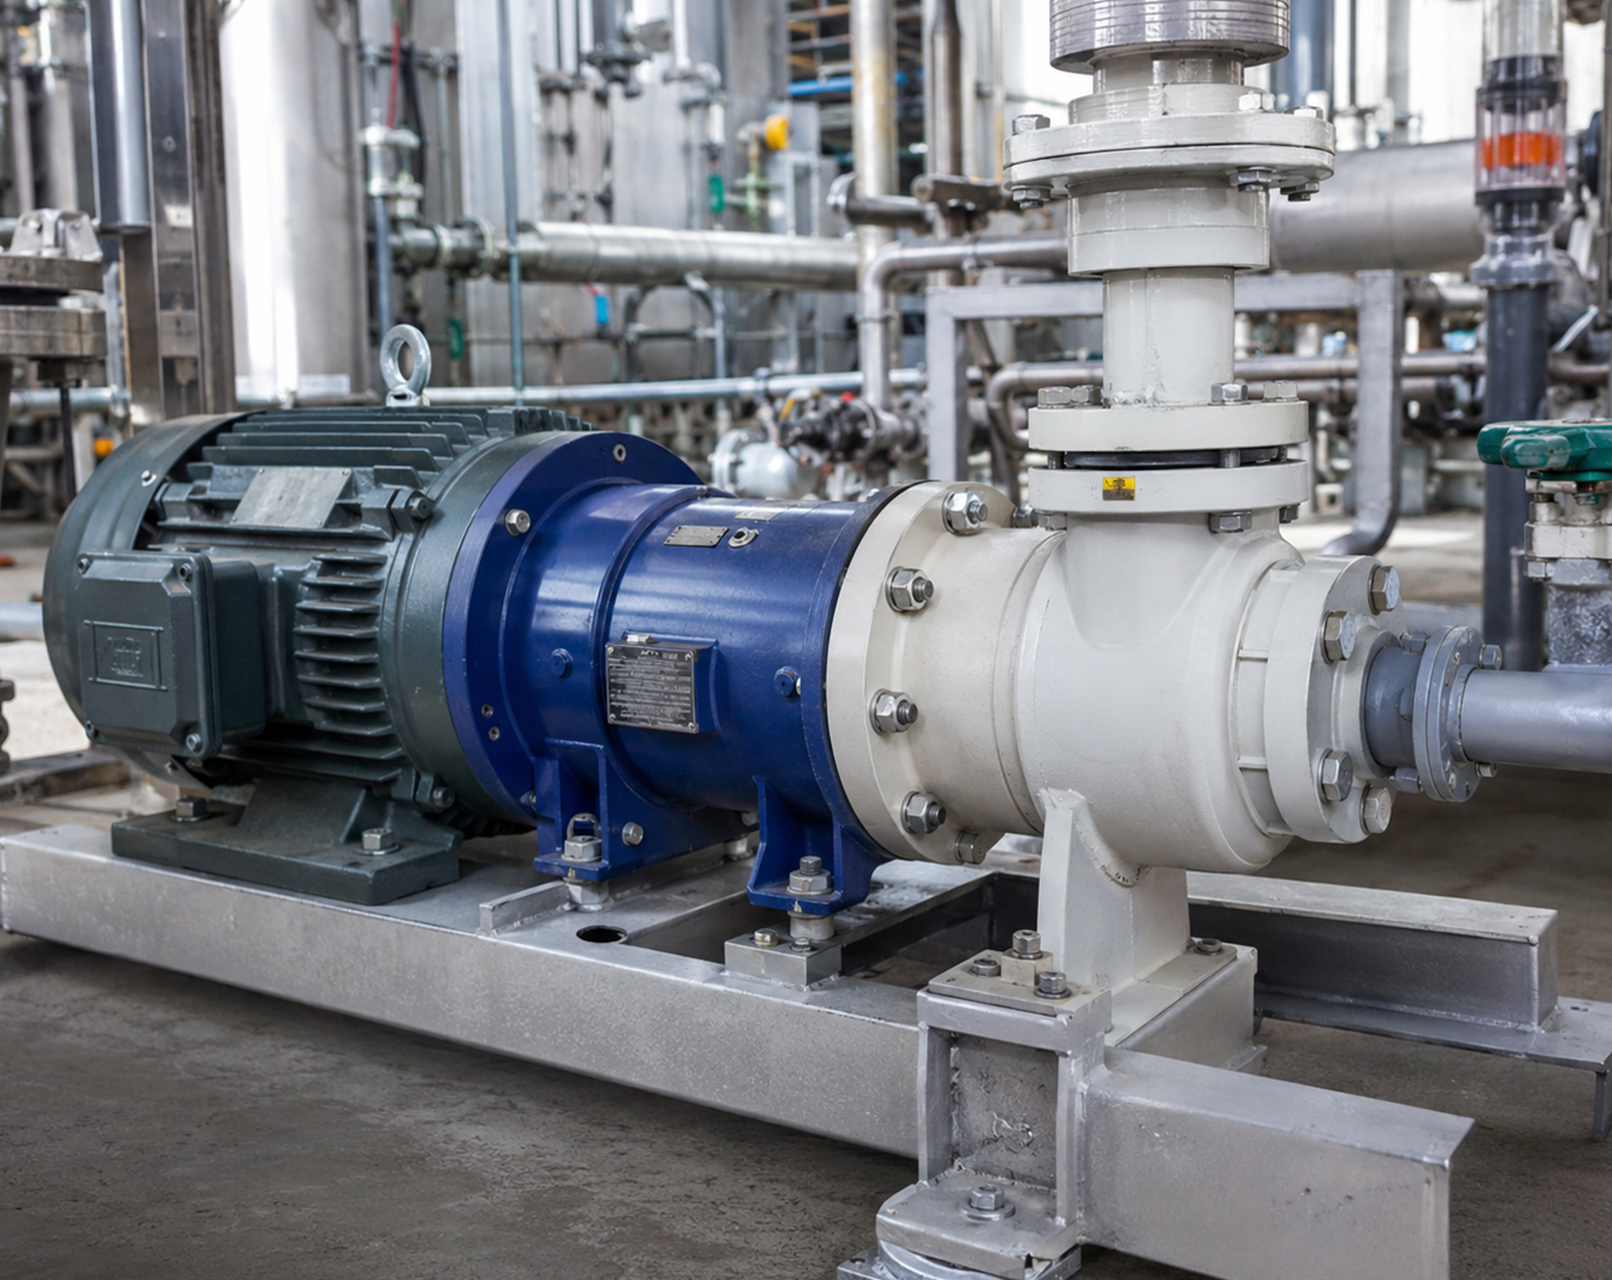
Chemical Pumps
Chemical Pumps

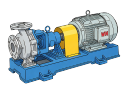
HRZL Industrial Pump

Features & Benefits

Built to match different fluids, duty points and industrial operating conditions with reliable performance and practical maintenance.
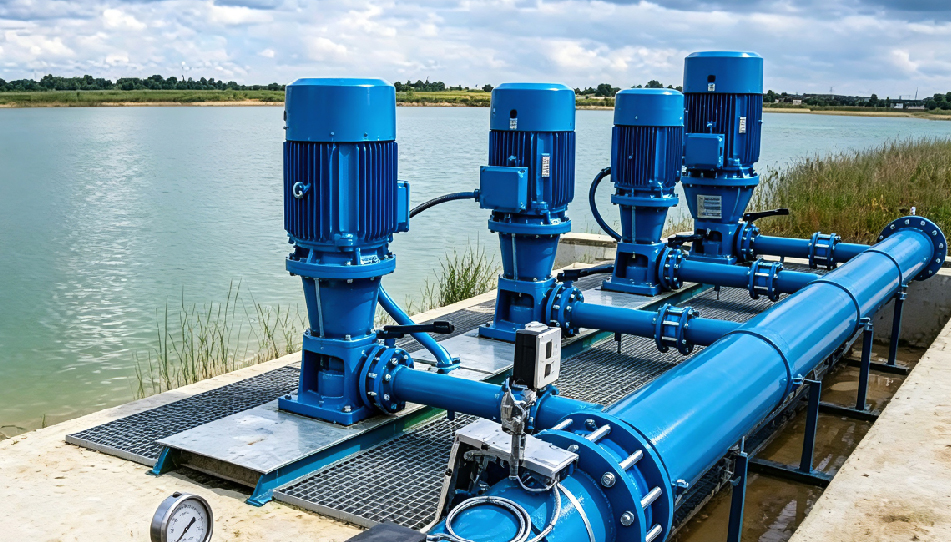
Pump Selection for Your Application
Pump type and configuration are selected based on flow, head, fluid properties and operating conditions.
Materials Matched to the Fluid
Cast iron, stainless steel, duplex and other materials are selected for water,chemicals.corrosive liquids and abrasive fluids.
High-Flow & High-Head Capability
Pump configurations are available for large-flow water transfer high-head systems and demanding industrial duties.
Built for Continuous Industrial Operation
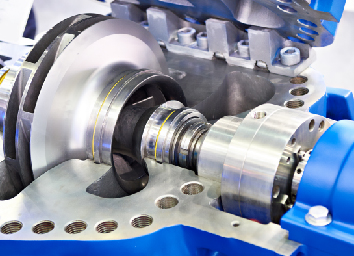
Heavy-duty shafts, bearings, seals and pump structures are designed for stable long-term operation.
Pump Packages for Your Site
Electric, diesel, skid-mounted and other package options are configured according to installation and site requirements.
Factory-Tested Before Delivery
Flow, head, running condition and key performance data are checked before shipment to verify the required duty point.

Factory Testing for Industrial Pump

Every Industrial Pump is tested before delivery to verify hydraulic performance, mechanical stability and the required duty point.
Cold Run &
Vibration Monitoring
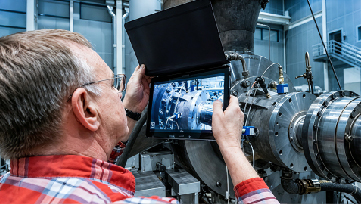
Vibration, noise and temperature are monitored to verify smooth and stable operation.
Hydraulic Performance
Verification
Flow, head, input power and efficiency are checked against the required duty point.
Full-Load Performance
Test
The pump is operated under specified load conditions to verify performance and running stability.
High-Temperature &
High-Pressure Testing
Critical-duty pumps can be tested under elevated temperature and pressure conditions.
Final Performance
Validation
Key operating data, leakage, vibration and mechanical condition are recorded and verified.
Cold Run &
Vibration Monitoring
Vibration, noise and temperature are monitored to verify smooth and stable operation.

Industrial Pump in Real Projects

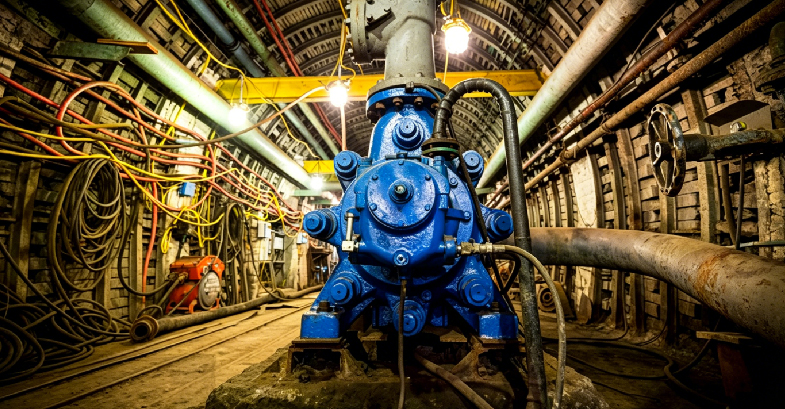
Mine Dewatering

Mine Dewatering

450 m³/h @ 760 m Head

High-head multistage pump for underground mine water removal.
· Mine Water
· MD450-95×8(P)
· Factory Tested
Chemical Processing

Chemical Processing

100 m³/h @ 50 m Head

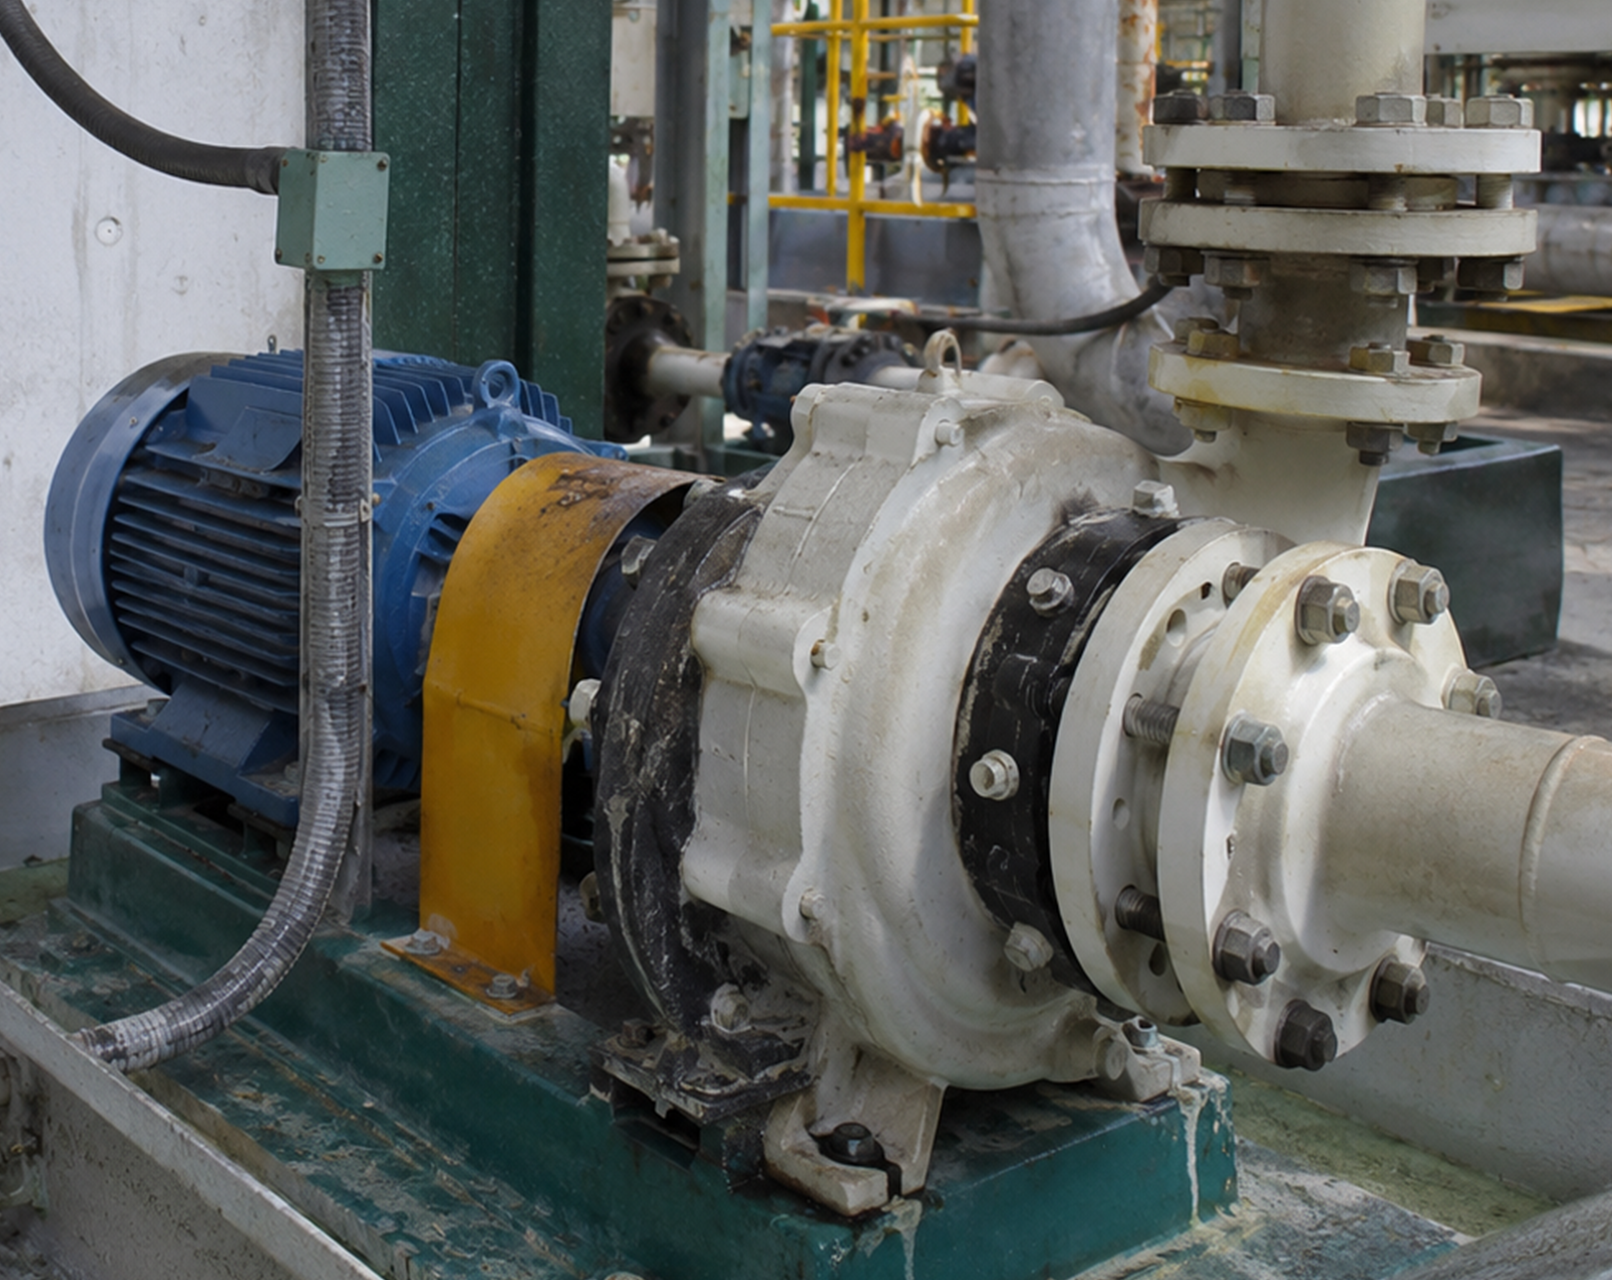
Corrosion-resistant chemical pump for industrial chemical transfer.
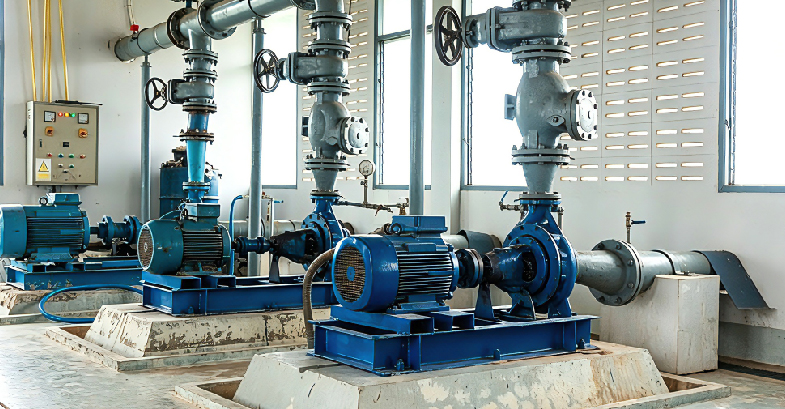
· Corrosive Liquid
· IH100-65-200
· SS316L / Factory Tested
Power Plant Cooling Water

Power Cooling Water

2020 m³/h @ 59 m Head

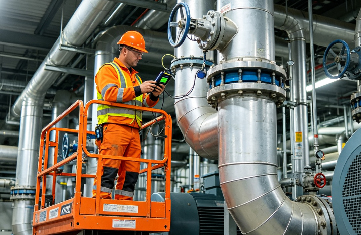
High-flow split case pump for continuous power plant cooling-water circulation.
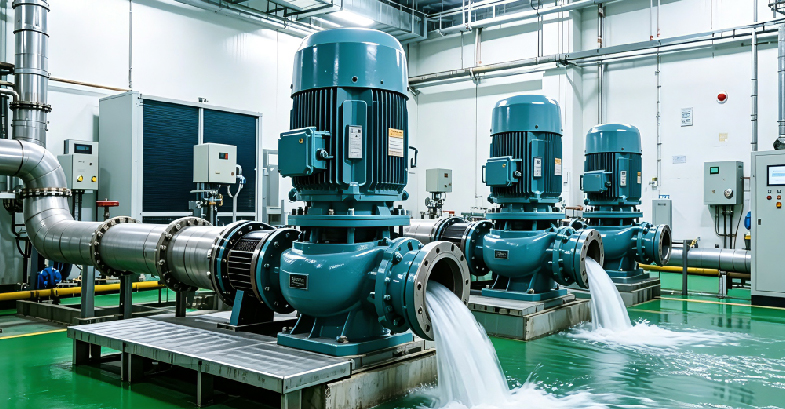
· Cooling Water
· 500S59
· Factory Tested
Raw Water Intake

Raw Water Intake

1200 m³/h @ 45 m Head

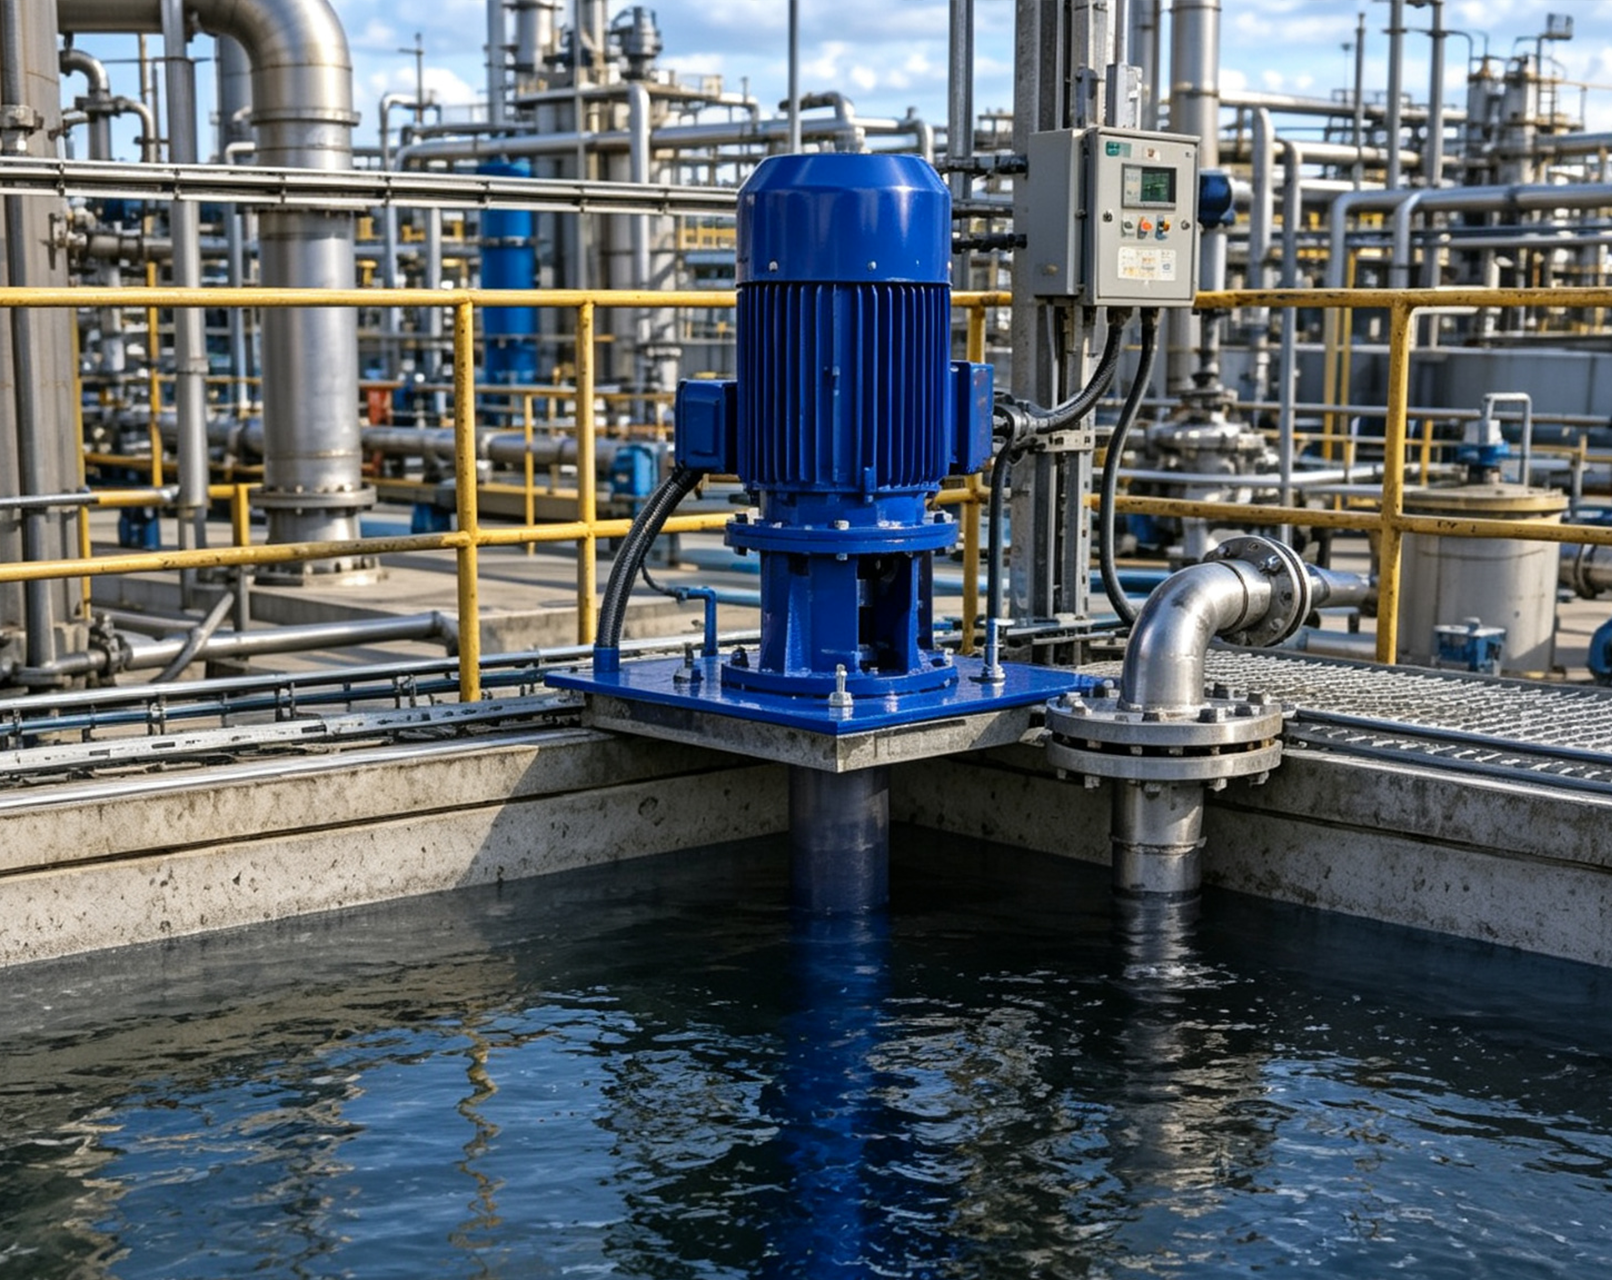
Vertical turbine pump for raw-water intake from deep wells and reservoir intake structures.
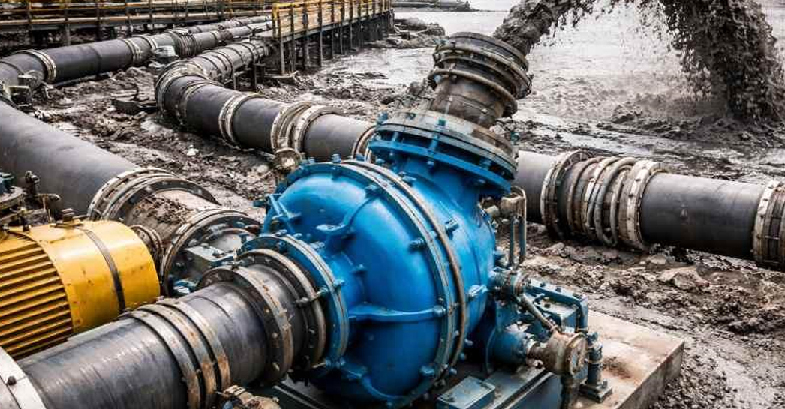
· Raw Water
· 400VTP Series
· 15 m Installation Depth / Factory Tested
Tailings & Slurry Transfer

Tailings & Slurry Transfer

436 m³/h @ 44 m Head

Heavy-duty slurry pump for abrasive tailings and high-solids slurry transfer.
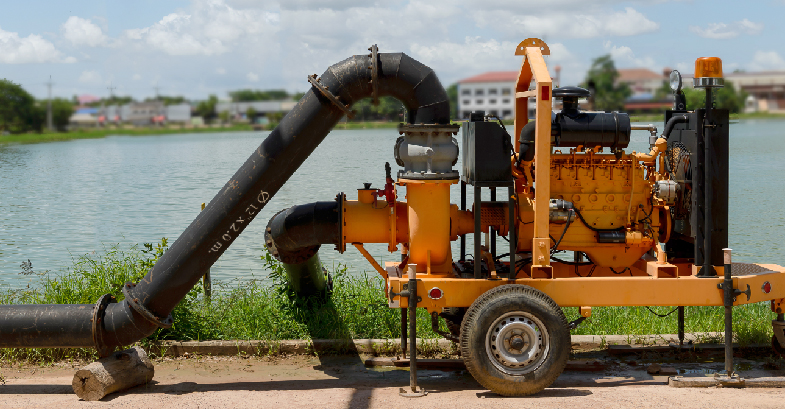
· Tailings Slurry
· 8/6E-AH Series
· 25–40% Solids / Factory Tested
Remote Site Dewatering

Remote Site Dewatering

500 m³/h @ 38 m Head

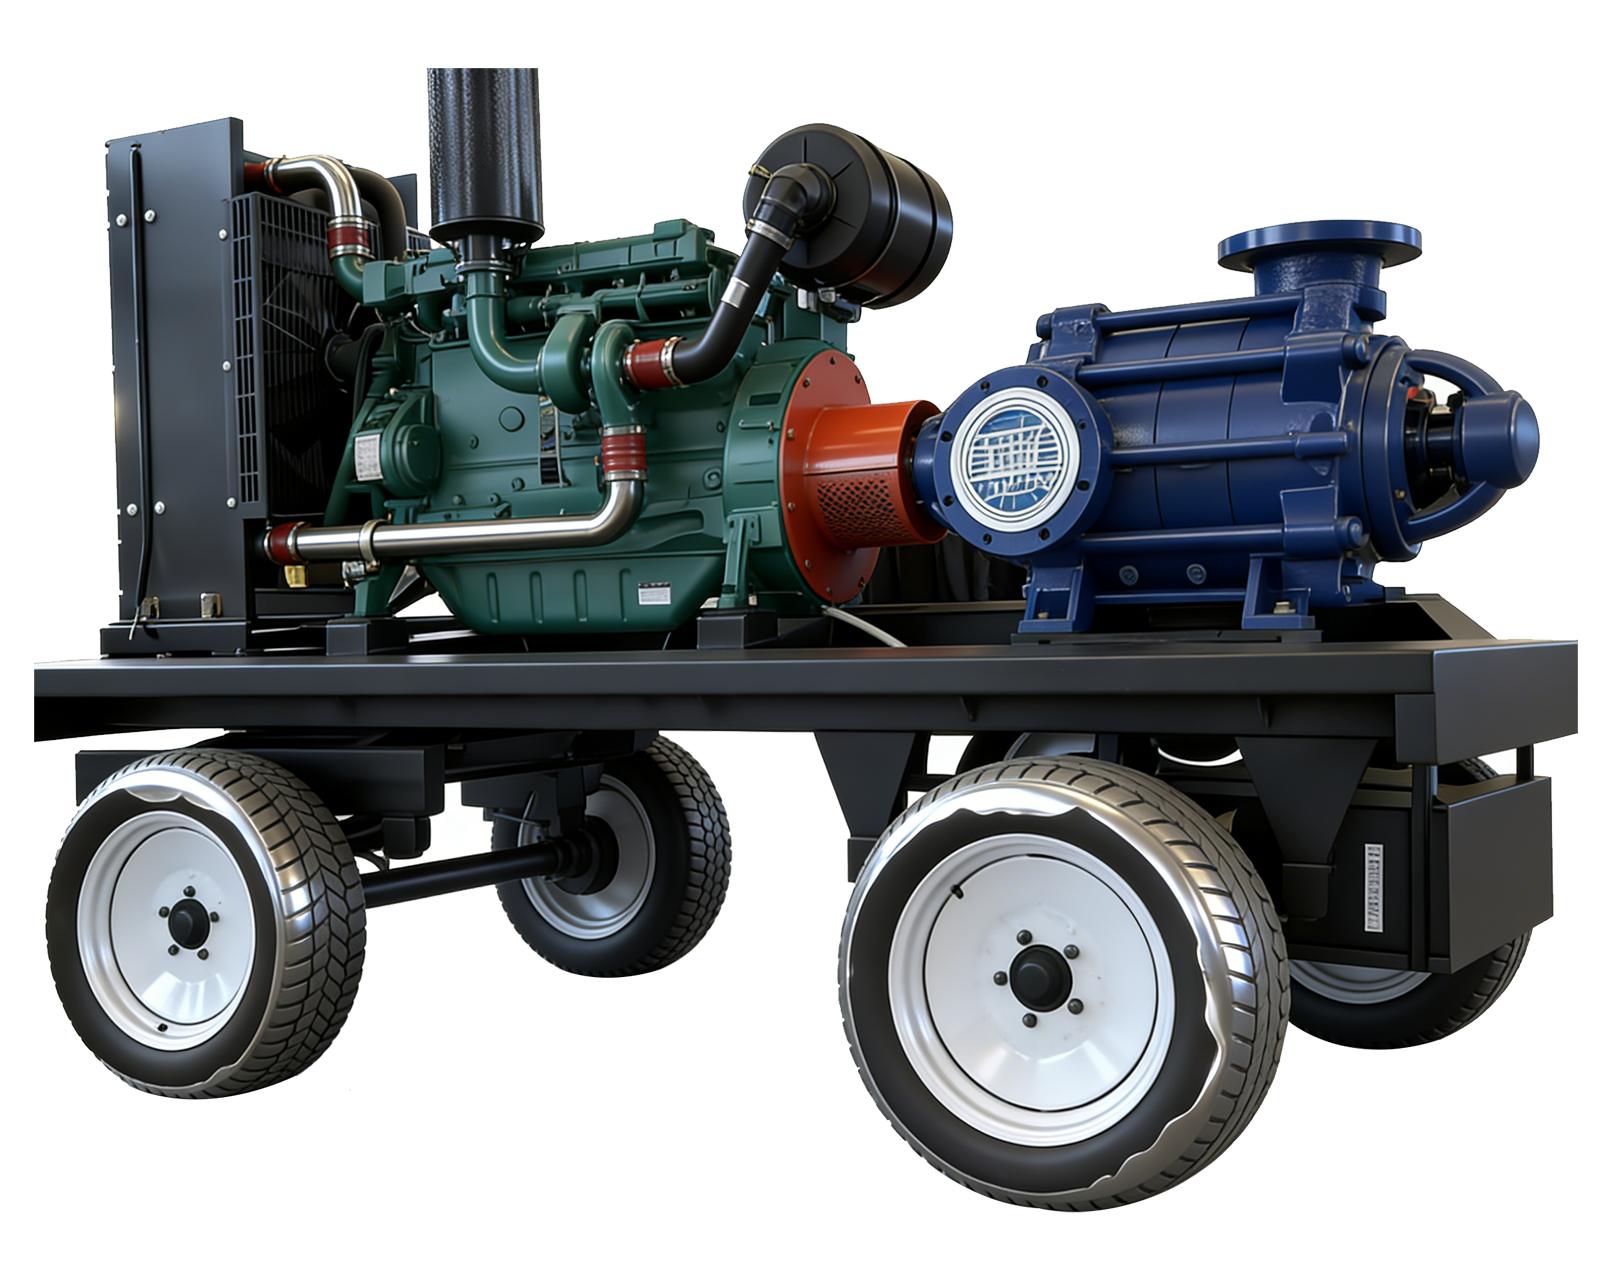
Diesel-driven pump package for remote dewatering and water transfer where grid power is unavailable.

· Dirty Water
· BA150E D285
· Trailer-Mounted / Factory Tested

Get the Right Industrial Pumps

Share your operating conditions to receive pump selection, technical data and a customized quote.
info@hrzlpumps.com
+86-15053308079
Get A Quote Price Icon WhatsApp WhatsApp Icon