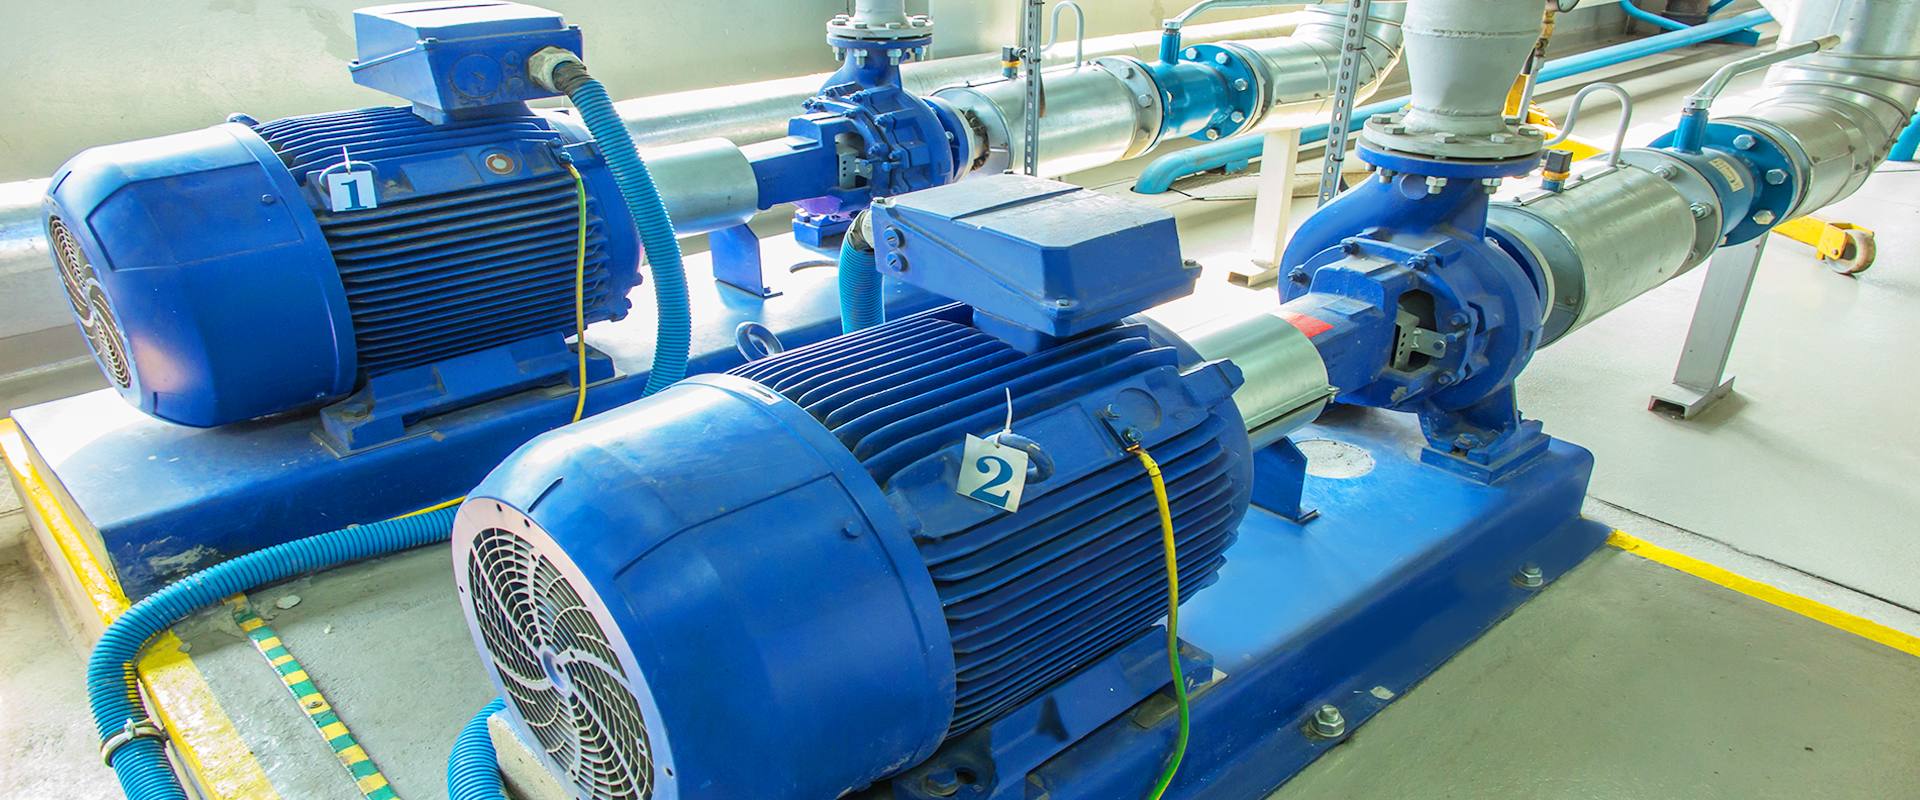
Chemical Pump
HRZL offers customers a wealth of design features, corrosion-resistant materials and material application expertise. Our technologies provide safe, reliable, environmentally friendly and lifecycle solutions for demanding chemical applications. Our solutions for the chemical process industry include pumping, separation and mixing, as well as rotating equipment and infrastructure services. We have extensive experience in the production of chemicals, plastics and pharmaceuticals, as well as the processing of renewable materials.
Related Products
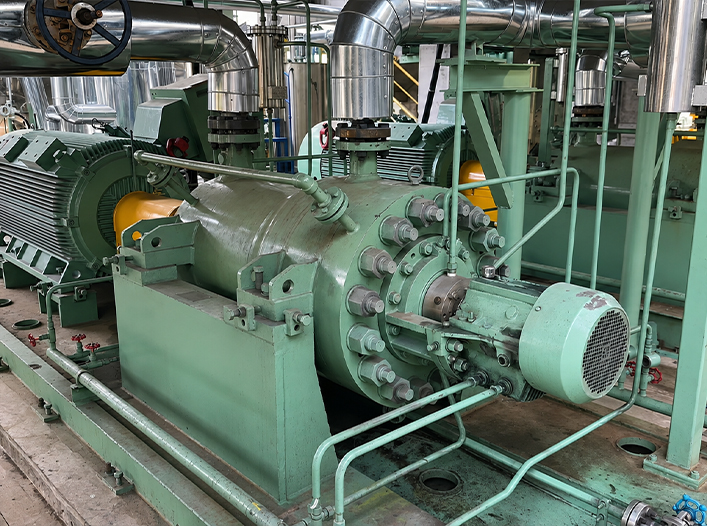
oil/gas/petrochemical
HRZL-BB5 API 610 BB5 High Pressure Barrel Pump
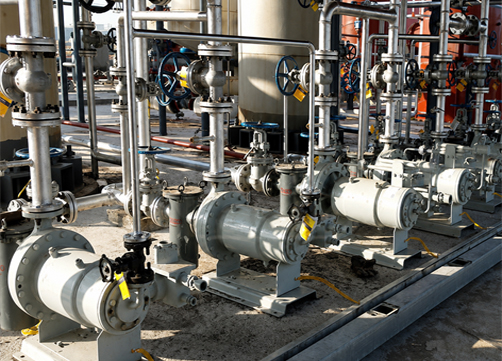
Toxic/Flammable/Hazardous/Liquids
HRZL-EX Canned Motor Pump
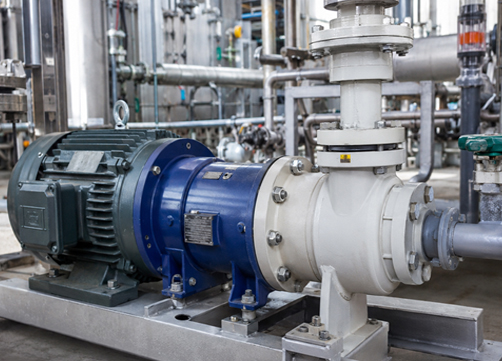
Strong Acids/Alkalis/Corrosive Chemicals
HRZL-IHF Fluoroplastic Chemical Pump
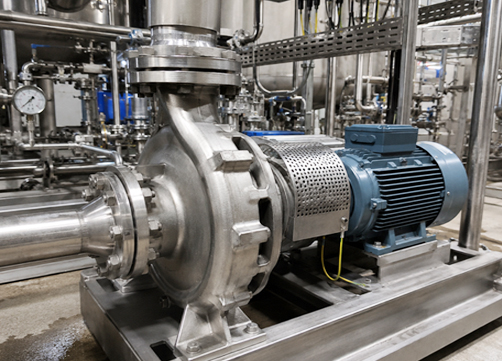
Corrosive/Chemical Liquids
HRZL-IH Stainless Steel Chemical Pump
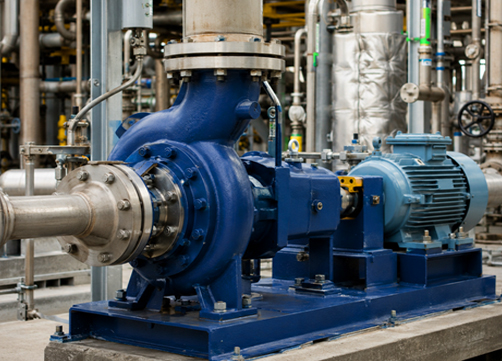
Corrosive/Process/Industrial Chemicals
HRZL-CZ Chemical Process Pump
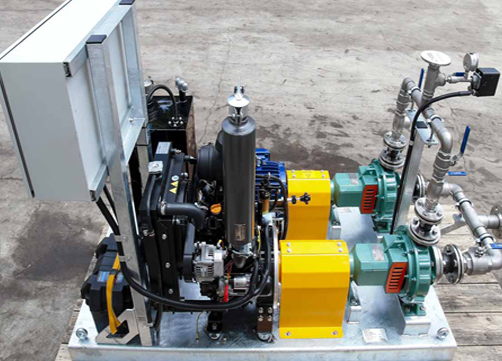
Acids/Alkalis/Corrosive Chemicals
HRZL-ZK Corrosion-Resistant Pump
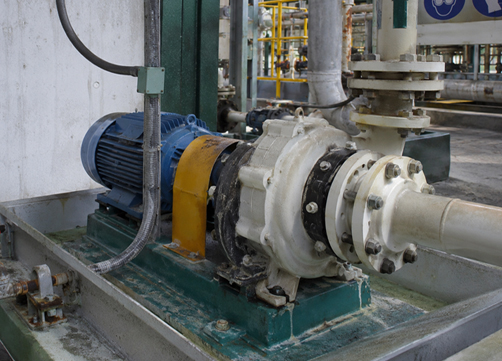
Corrosive/Toxic/Volatile Chemicals
HRZL-ZMD Magnetic Chemical Pump
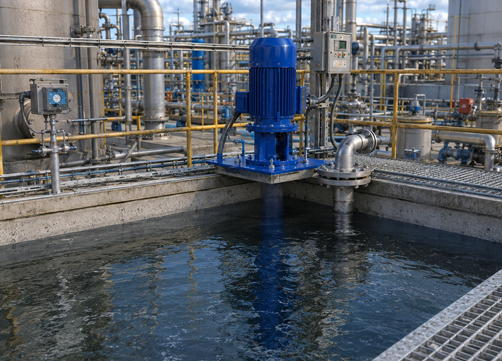
Corrosive/Chemical Liquids
HRZL-LW Vertical Chemical Pump
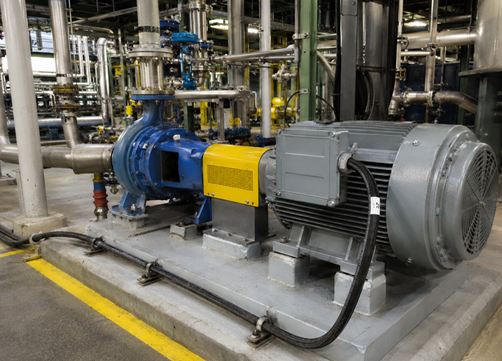
Chemical Processing / Industrial / Petrochemical
HRZL-IH IH Chemical Pump
Chemical Pump applications
The Benefits Of Chemical Pump
Safe and efficient pumping solutions for handling corrosive and hazardous chemicals.
Made with materials to resist acids, alkalis, and solvents.
Sealed systems prevent toxic leaks and environmental harm.
Delivers accurate dosing for chemical processes.
Handles hot fluids in demanding industrial applications.
Safe for use in flammable or hazardous zones.
Long service life even under aggressive chemical exposure.
Call for Sales or Support
If you need help with Pump Selection, Sales or Engineering Support Call +86 15053308079
Contact